Published: 18 October 2026
Last Updated: 18 October 2026
Reading Time: 16 minutes
Written by: [Author name and relevant credentials]
Technically Reviewed by: [Reviewer name and credentials]
Editorial and Technical Disclosure:
Published by S&M Co. Ltd. / Shenzhen Chuxin Electronic Equipment Co., Ltd. No individual author or technical reviewer is identified for this guide. The article is an informational overview, not a statement of production qualification, safety certification, regulatory approval, or independent process validation.
Technical recommendations should be checked against applicable standards, equipment documentation, material supplier guidance, workplace safety requirements, and the reader’s own process data.
Reading time is estimated at approximately 16 minutes, based on about 3,200 words at 200 words per minute. This is provided as a convenience estimate, not a measure of technical rigor or completeness.
No first-hand testing or production observation is claimed in this article unless specifically identified in the text.
Commercial interests: None disclosed.
Introduction: Why Selective Soldering Settings Cannot Be Chosen in Isolation
You have a board full of through-hole components. Some joints look perfect. Others? Insufficient barrel fill, bridges between pins, maybe a scorched component nearby. And your cycle time keeps bouncing around.
You’re not alone in this. This is the exact situation facing every selective soldering line in consumer electronics, semiconductor modules, automotive controllers, military assemblies, and aerospace hardware. And here’s the uncomfortable truth: there is no magic recipe sitting in a spreadsheet somewhere that you can copy and paste onto your machine.
The best selective soldering settings form a validated process window, not a universal set of numbers. Your board is different. Your components have different thermal mass. Your alloy, flux, nozzle, and machine all play together in ways that are unique to your setup. What works for one product family will fail on another.
So what actually works? A systematic workflow. You need to define your acceptance requirements first. Then establish a baseline. Calculate starting values. Profile the assembly. Run designed trials. And lock the process with statistical controls.
This guide walks you through that workflow step by step. We cover the IPC standards you need to know, how to calculate defensible baseline settings from manufacturer data, how to profile your real assembly, how to run DOE trials that actually give you answers, how to diagnose defects when they happen, and how to lock everything down with SPC and change control.
Let’s get into it.
About the Author
No individual author credentials have been supplied for this guide. The publisher has not identified a named author or technical reviewer with verified selective soldering experience, SMT production line background, lead-free process engineering credentials, thermal profiling expertise, or electronics manufacturing quality qualifications.
The placeholder format below must remain until substantiated details are available:
“[Author name] is [verified role/credential] with [verified experience] in [relevant soldering, SMT, or electronics-manufacturing specialty]. [He/She/They] has [specific, verifiable achievement or responsibility related to selective soldering process development.]”
Readers seeking author-identified content should request a fully attributed version with verifiable employment history, relevant certifications, publication record, and conflict-of-interest disclosures before applying any recommendations to production decisions.
This section will be updated when author information becomes available.
1. Start With the Product, Materials, and Acceptance Requirements
Before touching a single machine setting, you need to know exactly what you’re working with. Sounds obvious, right? But here’s the thing: most selective soldering problems I see start with incomplete input specs.
Your board design drives everything. PCB thickness, copper distribution, thermal planes, hole-to-lead ratio, component temperature limits, shadowing risk, pallet constraints, and target takt time. All of these constrain your process window. Skip this step and you’ll spend weeks chasing problems that were baked in from the start.
Map your thermal mass across the assembly. Thick copper pours absorb heat fast. Fine-pitch components next to large connectors? Different thermal zones. You need to know which joints will be hardest to fill and which components might shadow their neighbors.
Document your consumables too. Alloy liquidus and recommended pot temperature range, flux chemistry and solids content, board surface finish, component-lead finish, and whether you’re running nitrogen. Each one shifts your process window. The latest J-STD-001J and IPC-A-610J documents (January and March 2024 respectively) make clear that material selection isn’t separate from process validation. It’s part of it.
Now pull your acceptance criteria. IPC-A-610 Class 2 typically requires around 50% vertical barrel fill. Class 3 pushes that to 75% minimum. But don’t just quote the class. Your customer drawings, military controls, or aerospace requirements might tighten those numbers further. NASA and spaceflight applications typically enforce the stricter 75% minimum fill regardless of general IPC class.
Create a simple reference that ties every input to a measurable output and where that data comes from:
| Input Factor | Measurable Response | Data Source |
|—|—|—|
| PCB thickness | Thermal ramp rate capability | Design spec |
| Copper distribution | Preheat uniformity | Thermal simulation |
| IPC class | Minimum barrel fill % | IPC-A-610J |
| Flux solids content | Activation window | Flux datasheet |
| Component limits | Peak temperature cap | Component spec |
This input checklist becomes your baseline. Once constraints are known, the machine variables can be mapped to their physical effects.
Practical Consideration: Print this checklist. Walk it through the product engineering team before your first trial. Missing one thermal plane on a power board can waste an entire qualification cycle.
2. Understand What Each Selective Soldering Parameter Controls
Now that you know your product requirements, let’s look at what each machine setting actually does. Every parameter has a physical effect on your joints. Get one wrong and you’ll see the results as a specific defect type.
Here’s the core reference that ties settings to physical effects and defect outcomes:
| Parameter | Unit | Physical Effect | Evidence to Set It | Defect Risk When Low | Defect Risk When High |
|—|—|—|—|—|—|
| Flux deposition | mL or shots | Activation energy, surface oxide removal | Flux datasheet activation window | Non-wetting, skips | Residue, bridging, spread |
| Preheat temperature | °C | Thermal ramp, flux activation, component protection | Component peak limit, flux activation range | Cold joints, poor fill | Component damage, excessive oxidation |
| Solder pot temperature | °C | Alloy fluidity, wetting force, heat delivery | Alloy liquidus, copper dissolution rate | Insufficient fill, cold joints | Copper dissolution, dross, icicles |
| Wave height | mm | Solder volume available per contact | Joint geometry, fill requirement | Insufficient barrel fill | Bridging, icicles, solder balls |
| Pump speed | % or rpm | Wave turbulence, flow dynamics | Nozzle geometry, pitch density | Poor solder mobility | Turbulence, splashing, bridging |
| Immersion depth | mm | Contact area, heat transfer rate | Thermal mass of joint | Insufficient heating | Bridging, pad damage |
| Contact/dwell time | seconds | Heat input, solder fill duration | Barrel fill requirement, component limits | Insufficient fill | Copper dissolution, icicles, component stress |
| Traverse speed | mm/s or mm/min | Cooling rate, path time, cycle time | Joint density, throughput target | Uneven heating | Insufficient dwell, skips |
| Nitrogen flow | L/min or ppm O2 | Atmosphere oxygen level, oxidation control | Flux compatibility, finish sensitivity | Oxidation, poor wetting | Cost, unnecessary consumption |
Flux settings: enough activation, not too much spread
Flux does two things. It cleans oxide from surfaces and it provides chemical energy to help solder wet the metal. Too little flux and you get non-wetting or skips. Too much and you get residue buildup, bridging between pins, or flux spreading where it shouldn’t go.
Drop-jet flux systems give you precise control over where each shot lands. Spray flux covers larger areas but needs careful pattern setup. Your flux datasheet tells you the activation temperature window and how much solids content you need for reliable wetting.
Expert Tip: Machine commands for flux volume and wave height are starting points, not verified reality. Physical verification of actual deposited quantity and measured wave height at operating temperature is essential before trusting nominal machine settings.
Thermal settings: preheat protects and prepares
The preheat stage does three jobs at once. It drives off solvents in the flux. It starts the activation chemistry. And it brings the board and components up to a temperature that prevents thermal shock when they hit the hot solder wave.
Bottom preheat heats the board from underneath. Top preheat targets component bodies and leads. You set these as temperature setpoints or power percentages depending on your machine.
The relationship between preheat and wetting is direct. A cold board steals heat from the solder wave on contact. The result is sluggish wetting and poor barrel fill. Too much preheat and you risk component damage or flux burn-out before the solder even arrives.
IPC-7530 is the thermal profiling standard you should follow. Profile your hottest and coldest board locations to find the real temperature spread across your assembly.
Contact and flow settings: where the action happens
Once the board reaches temperature, it meets the solder wave. This is where nozzle geometry, wave height, pump speed, and immersion depth all interact.
Nozzle shape controls the wave profile. Smaller nozzles focus solder delivery for tight areas. Larger ones cover more ground but risk bridging at close pitches.
Wave height sounds simple, but it’s where a lot of recipes go wrong. The machine may command a height, but the actual wave at operating temperature depends on pump speed, solder level in the pot, and nitrogen atmosphere. Measure it physically with a wettable coupon or glass plate at your actual process conditions.
Pump speed drives wave turbulence. Higher speeds mean more energetic flow, which helps solder get into tight holes. But aggressive turbulence can splash solder onto mask and cause bridging at fine pitches.
Immersion depth is the vertical distance the nozzle sits below the board surface. Deeper immersion means more contact area and more heat transfer. But it also means more solder exposure and higher bridging risk. Most operators under-estimate how much this parameter affects results.
The approach path and withdrawal behavior control peel-off. A clean break at the end of each solder contact prevents icicles and bridging. Board speed, solder angle, and the motion profile all combine here. This is where most recipe development time gets spent because these settings are interactive with each other.
Nitrogen flow reduces oxidation at the solder surface. Oxygen concentration targets vary by flux type and solder alloy, but typical settings fall between 50 and 500 ppm at the nozzle. Check your flux and alloy supplier specifications.
Keep-out clearance is a geometry constraint, not a process variable, but it still matters. If the nozzle sits too close to adjacent components, you get shadowing on one side and potential collision damage on the other. Map your keep-outs carefully before programming any path.
3. Calculate Safe Baseline Settings Before the First Trial
Before you program a single path or touch the machine, you need a defensible starting point. That means doing the math before you make smoke. This section shows you how to calculate heating time, contact time, and thermal rate from first principles, then build a baseline parameter sheet that survives scrutiny.
Calculate Available Heating Time
The board travels through the preheat zone before it reaches the solder wave. The heating time available is determined by the heated path length and the traverse speed.
Equation 1: Available heating time = heated path length (mm) / travel speed (mm/s)
If your speed is in mm/min, convert first: t = 60L/v
For example, if your heated path is 200 mm and your traverse speed is 8 mm/s:
t = 200 mm / 8 mm/s = 25 seconds of heating time available
Estimate Required Average Heating Rate
Now compare that against what the board actually needs. Starting from your measured or estimated board temperature entering preheat, calculate the temperature rise required to reach your target pre-solder temperature.
Equation 2: Average heating rate = temperature rise (°C) / elapsed time (s)
Using our example: if the board starts at 25°C and needs to reach 110°C before solder contact:
Rate = (110°C – 25°C) / 25s = 3.4°C/s
Check this against your laminate and component limits. Most high-Tg FR-4 materials tolerate ramp rates up to 2-3°C/s. If your calculated rate exceeds the limit, you need a longer heated path or slower traverse speed.
Calculate Solder Contact Time
Once the board reaches the solder wave, the actual contact time comes from the projected path length under the nozzle and the local travel speed.
Equation 3: Contact time = solder contact footprint (mm) / local travel speed (mm/s)
For a 30 mm contact path at 5 mm/s: 30 / 5 = 6 seconds. That’s probably too long for most lead-free applications. Most selective solder contacts run 1-4 seconds.
Practical Calculation Example
| Parameter | Hypothetical Value | Unit |
|—|—|—|
| Preheat zone length | 200 | mm |
| Traverse speed | 8 | mm/s |
| Available heating time | 25 | s |
| Board entry temperature | 25 | °C |
| Target pre-solder temperature | 110 | °C |
| Temperature rise required | 85 | °C |
| Required average heating rate | 3.4 | °C/s |
| Solder contact path length | 25 | mm |
| Local travel speed at wave | 6 | mm/s |
| Estimated contact time | 4.2 | s |
The 4.2-second contact time falls within the 1-4 second range commonly cited for lead-free selective soldering with SAC-type alloys. But this is a starting estimate. Your actual profile will differ due to thermal lag, conveyor behavior, and board-specific thermal mass.
Build the Baseline Parameter Sheet
Now compile your baseline from the narrowest overlap among all supplier limits. Each constraint narrows the window.
| Constraint Source | Parameter | Minimum | Maximum | Notes |
|—|—|—|—|—|
| Alloy (SAC305) | Pot temperature | 250°C | 270°C | Based on liquidus + margin |
| Flux activation | Topside preheat | 100°C | 130°C | Water-based flux window |
| PCB laminate (high-Tg FR-4) | Max ramp rate | – | 2°C/s | Supplier Tg limit |
| Component limits | Peak temperature | – | 260°C | Most lead-free ratings |
| Equipment | Min contact time | 1s | – | Practical mechanical limit |
| Equipment | Max contact time | 4s | – | Copper dissolution risk |
Use these as your locked boundaries, not your operating setpoints. The real optimum lives inside this envelope, and you’ll find it through profiling and DOE trials in the next sections.
The baseline sheet should include units, tolerances, assumptions, and revision control. Without that documentation, you have no traceability when something drifts.
Pro Insight: Cross-reference your flux datasheet activation window against your preheat settings before the first trial. A flux that needs 120°C minimum activation won’t work if your board only reaches 100°C at the solder wave entrance.
4. Verify the Thermal Profile and Solder-Wave Behavior on the Real Assembly
Your calculations give you a starting point. Now you need to prove that your machine actually delivers what the math says it should. That means profiling the board under real conditions and watching the solder wave behave.
Where to put your thermocouples
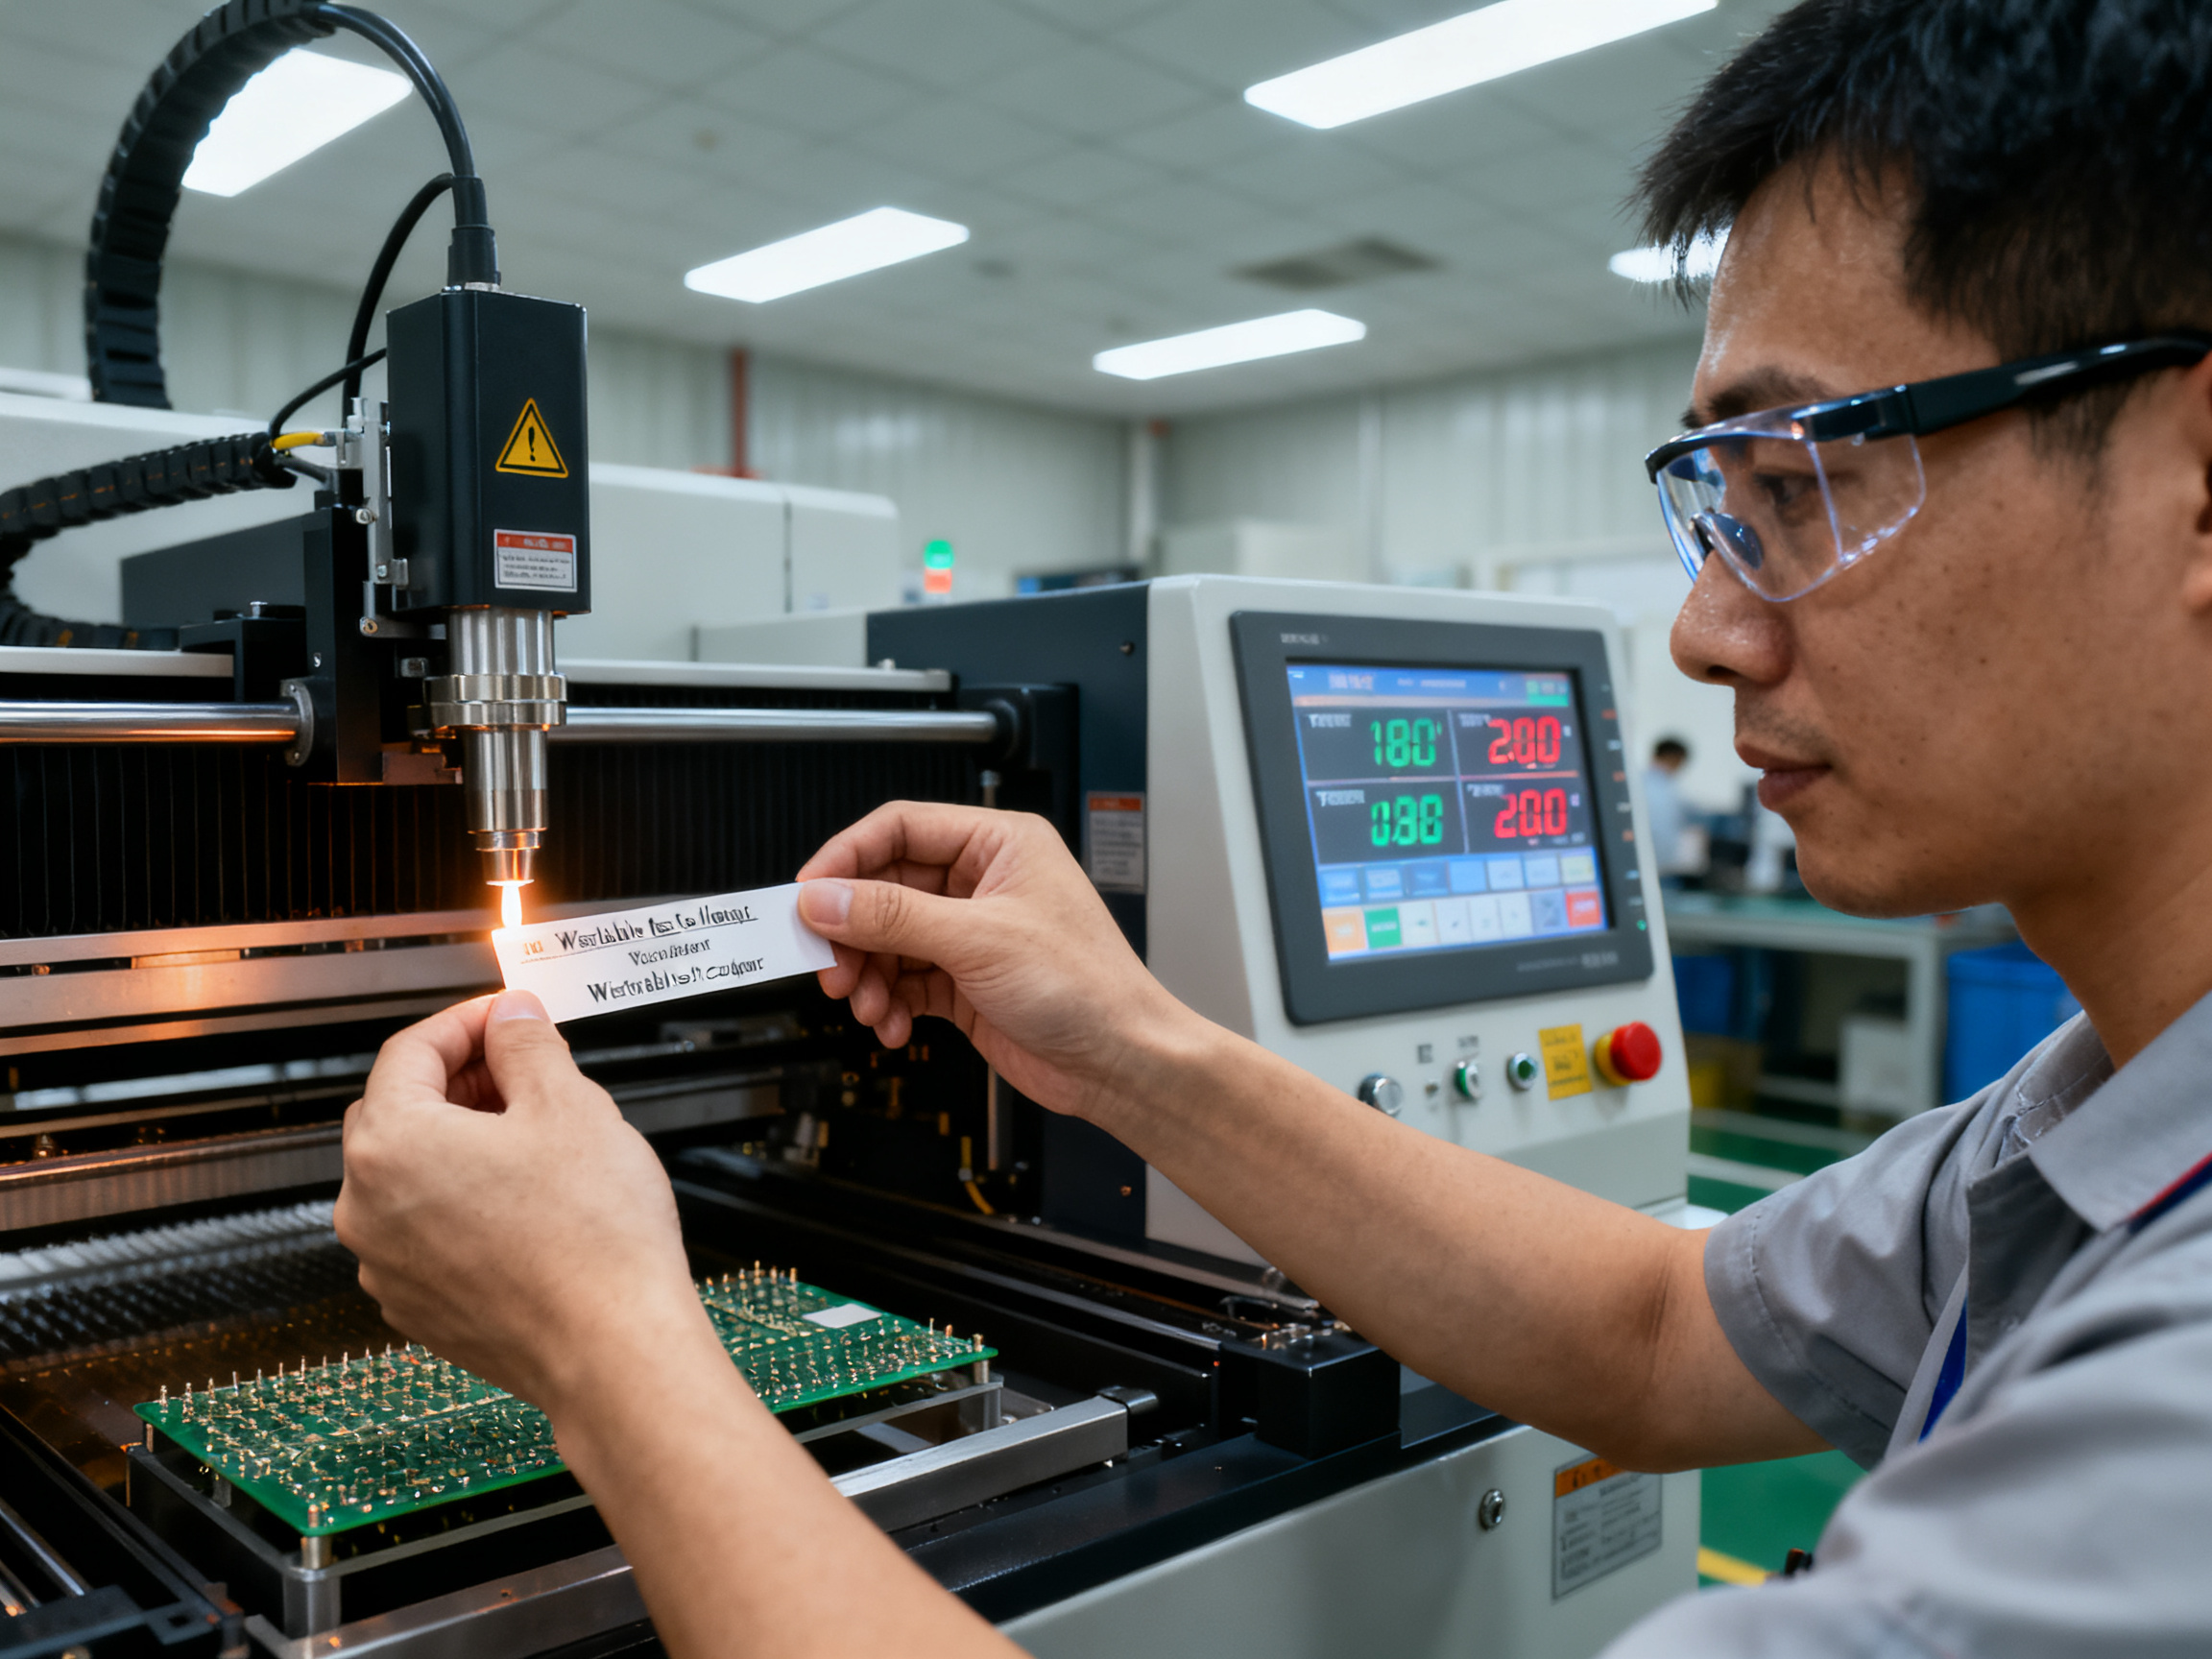
Grab your calibrated Type K thermocouples. Small wire, about 0.13 to 0.25 mm, keeps thermal lag to a minimum. Place them at the highest-mass joint, lowest-mass joint, temperature-sensitive component, board surface near where flux gets applied, and other spots that look risky. IPC-7530 is your reference for this work [1].
Attach each thermocouple with high-temperature solder or thermally conductive adhesive. Keep the junction flat against the surface. Route the wires away from the nozzle, wave, conveyor, and board edge. The goal is to measure what is happening where it matters, not where it is convenient to stick a wire.
What to evaluate from the profile
You need to look at ramp rate, flux activation duration, pre-solder temperature, peak and topside limits, time above liquidus, joint contact time, and cooling rate. Run your profile at about 10 samples per second. That is a solid default for selective solder work. Some faster transitions might need 20 or more, but 10 works for most applications [2].
The profile tells you whether your board actually reaches the temperature window your calculations predicted. If your hottest joint sits at 245°C and your coldest at 218°C, that 27-degree spread matters. You might need to slow down the fast joints or crank up heat for the slow ones.
Physical wave verification
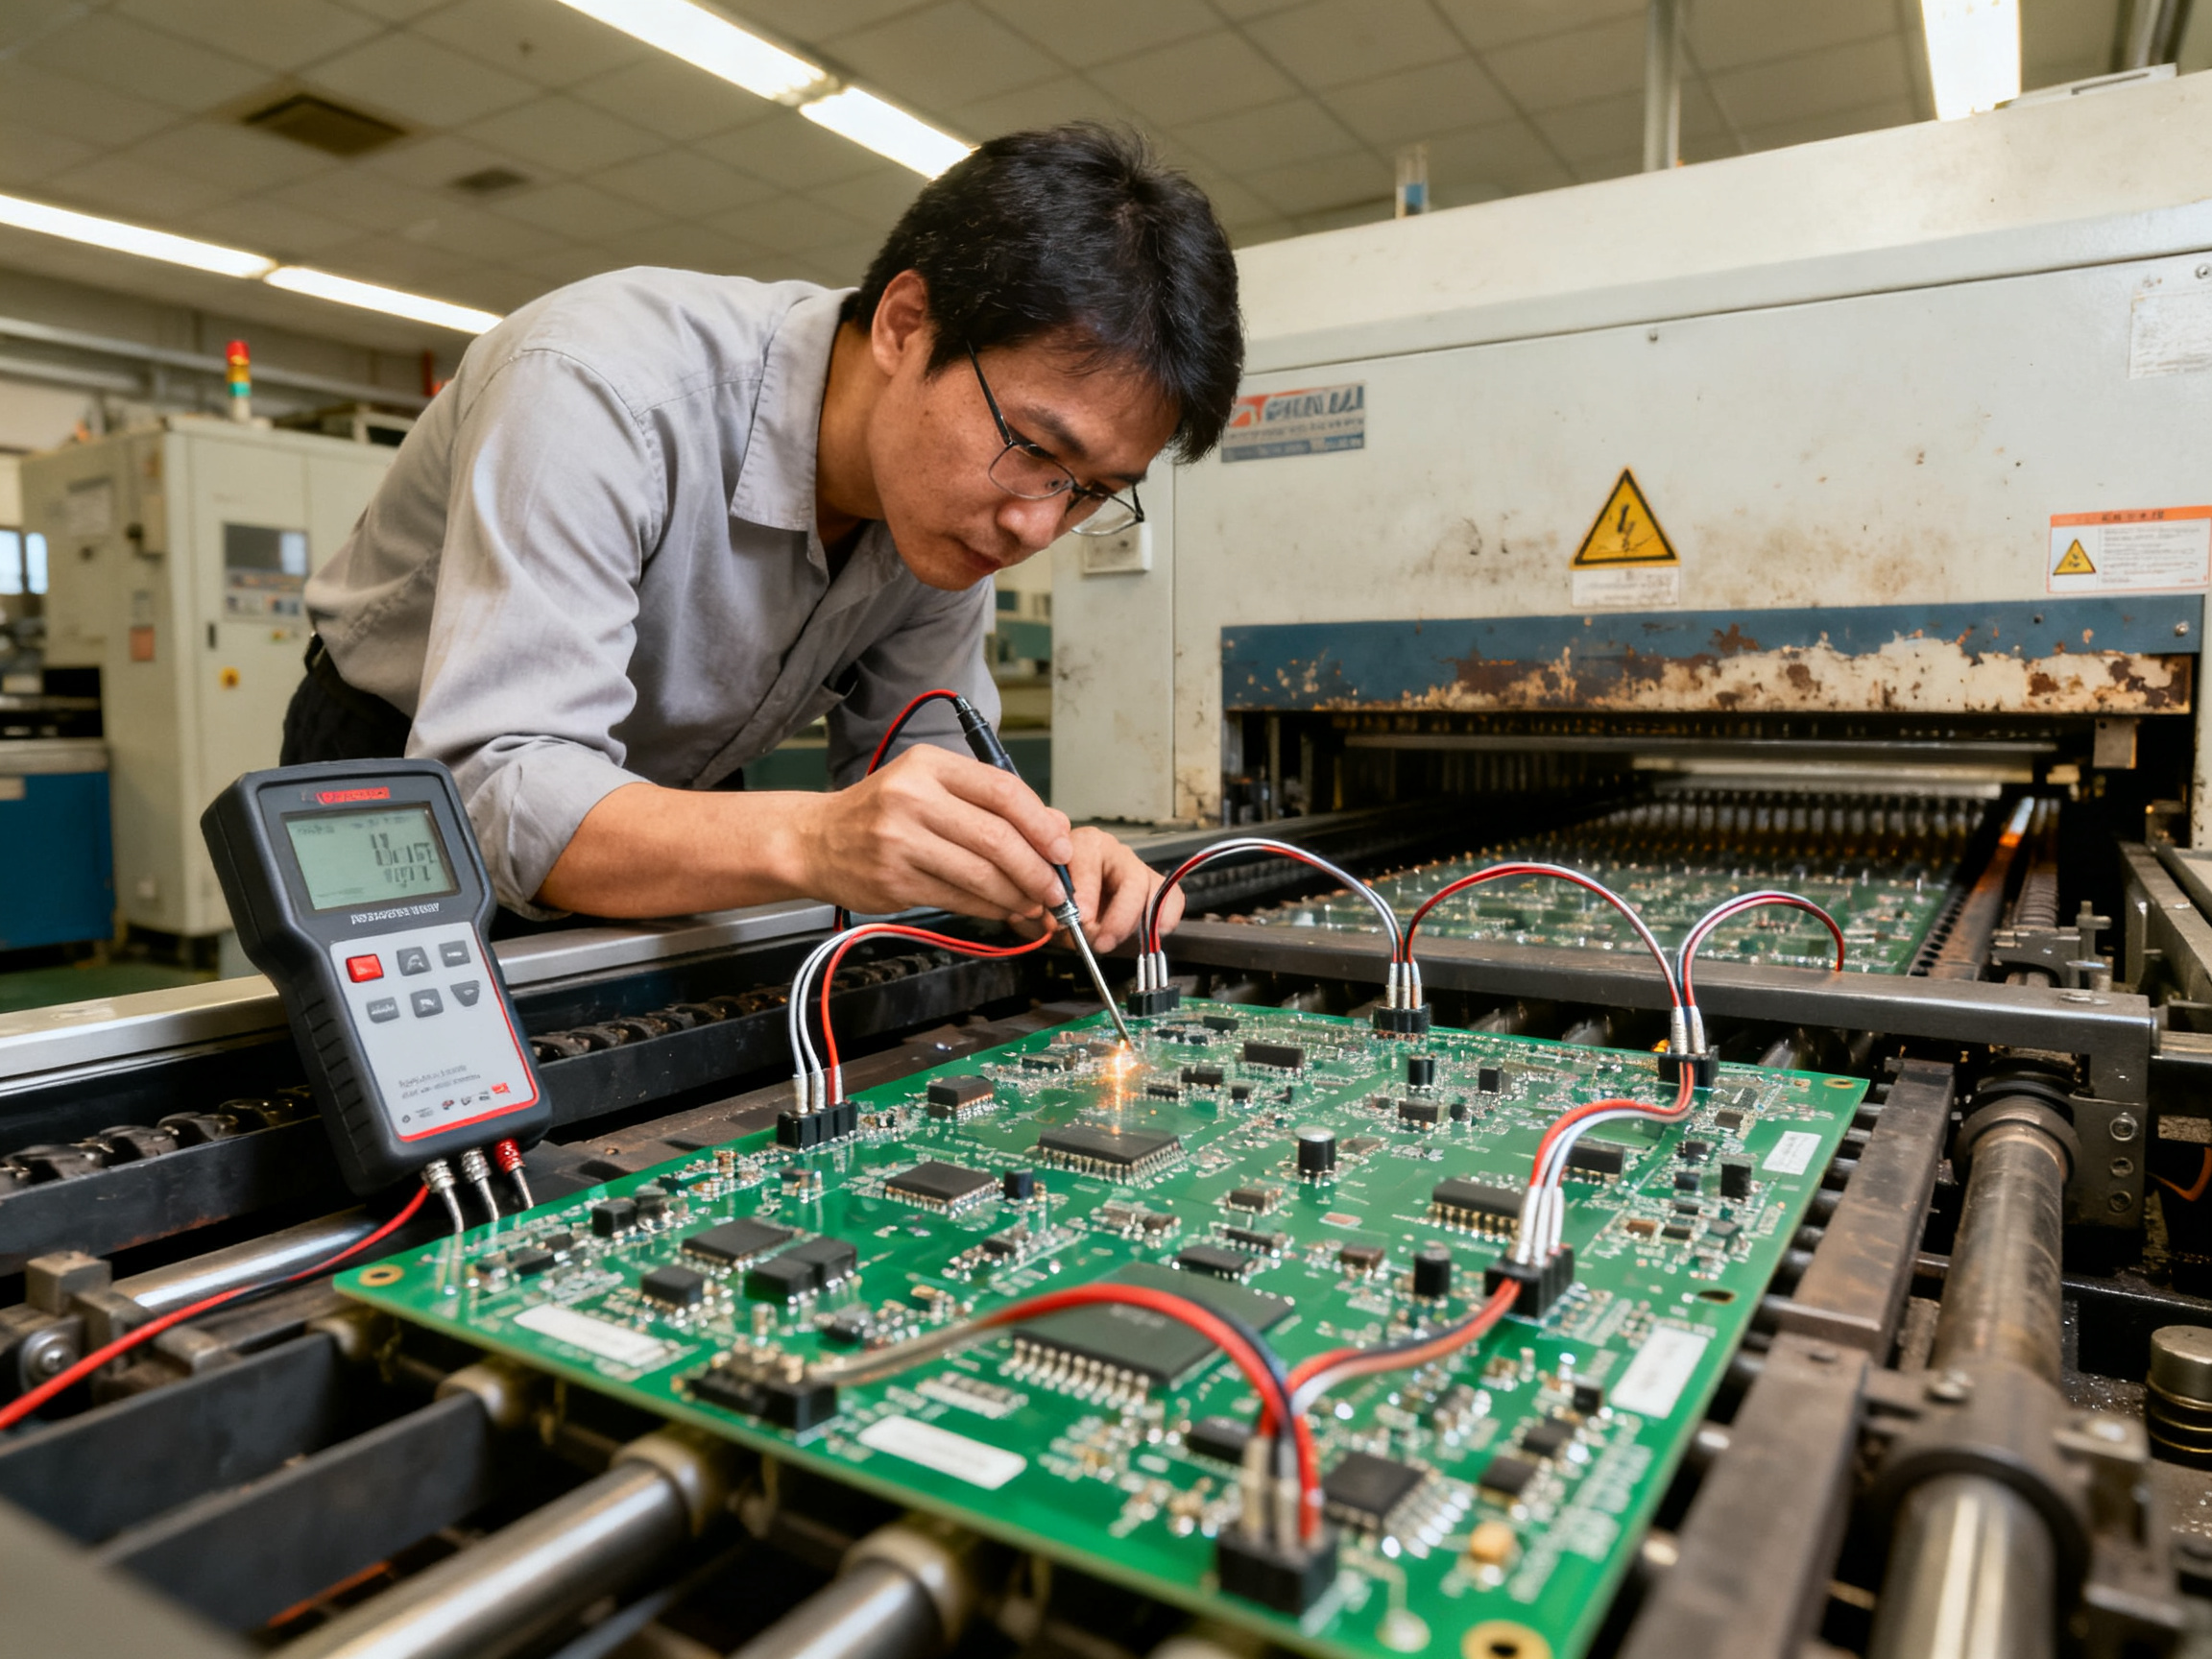
Now check the physical wave itself. Use a wettable coupon or glass plate at operating temperature to see the wave shape and height. Measure it at your actual pump speed, nitrogen condition, conveyor speed, nozzle configuration, and solder level [3].
Verify nozzle alignment relative to your programmed pad pattern. Check the X-Y offset, rotation, Z height, and board warpage. Look at your solder level and pot temperature. Check dross condition and removal frequency. And confirm your nitrogen flow and oxygen concentration at the nozzle region, not just at the generator.
From Our Experience: We once spent two days chasing intermittent barrel fill failures on a power board. The machine logs showed consistent pot temperature and dwell settings. The problem was solder level in the pot had dropped just enough that the wave height sagged at operating temperature. No alarm triggered. The wettable coupon test caught it in 20 minutes. Always verify the physical wave, not just the machine display.
Run at least three repeated profiles after any setup changes or maintenance. This confirms the process is stable. If your solder pot temperature reads 265°C on the display but your thermocouple at the joint shows 258°C, you have a gap to close before you trust the recipe.
Only by profiling the real assembly can you validate whether your baseline settings are safe and productive. This also builds the measurement system data you need for SPC and qualification later.
5. Optimize the Process Window With DOE, Not One-Factor Guessing
Here’s where most shops lose months of trial and error. They change one parameter at a time, log the result, move to the next, and never account for the fact that flux deposition interacts with preheat temperature, which interacts with wave height, which interacts with withdrawal speed.
One-factor-at-a-time testing misses interactions. It’s as simple as that. And in selective soldering, the interaction effects are often bigger than the main effects.
Set Up Your DOE Before Touching the Machine
A designed experiment starts with identifying your factors and levels. For selective solder process settings, your controllable factors typically include:
- Flux deposition volume or shot count
- Preheat energy (bottom zone temperature, top zone temperature)
- Solder pot temperature
- Pump speed or wave height command
- Dwell time or local travel speed
- Nitrogen flow rate and oxygen concentration
- Withdrawal speed and angle behavior
Each factor needs two or three realistic levels. You don’t need to test the entire manufacturer range. Pick a low, center, and high value that brackets your baseline from Section 3.
Hold nuisance variables constant or block them. That means using the same board revision, the same flux lot, the same nozzle, the same operator, and the same machine setup for all runs in the DOE. Any change you don’t control becomes noise in your data.
Define Your Responses Before Testing
Decide what you’re measuring before you run a single board. Vague objectives like “look better” don’t produce usable data. Instead, define responses that tie directly to acceptance criteria and production goals.
Your response list probably looks like this:
- Barrel fill percentage (from cross-section or X-ray)
- Bridge rate per 1,000 joints
- Skip rate per 1,000 joints
- Solder ball count per board
- Thermal limit margin (degrees below component rating)
- Pull strength or destruct test results where justified
- First-pass yield percentage
- Cycle time per board
Start With Screening, Then Refine
Run a screening DOE first. A Resolution IV fractional factorial or a definitive screening design lets you test 5 to 8 factors in a manageable number of boards while estimating main effects and two-factor interactions.
This is where most practitioners get surprised. The flux deposition by preheat temperature interaction often turns out to be significant. So does wave height by withdrawal speed. These interactions change which settings are actually optimal, and a one-factor experiment never finds them.
Once you’ve identified the 2 to 4 factors that actually matter, move to a response-surface design like a central composite design or Box-Behnken. This maps the curvature in your response and pinpoints the optimal region inside your baseline envelope.
| Response | Target | Lower spec | Upper spec | Measurement method |
|—|—|—|—|—|
| Barrel fill | >75% | 70% | 100% | Cross-section, X-ray |
| Bridge rate | 0 | 0 | 0.5% | AOI, electrical test |
| Skip rate | 0 | 0 | 0.2% | AOI, visual |
| Cycle time | <45s | 40s | 50s | Machine log |
Why a Centered Window Beats a Single Best Point
Here’s the critical part. When your DOE analysis finishes, resist the urge to pick the settings that gave your single best board. That result probably reflects random variation, a favorable board lot, or an interaction you haven’t captured yet.
Instead, select the centered process window. This is the region where:
- Mean response meets requirements with margin
- Variability is acceptably low
- Predicted response isn’t hypersensitive to small factor shifts
- The solution sits far enough from specification limits to survive material or environmental drift
A robust window keeps you out of trouble when flux lots vary, boards warp slightly, or ambient conditions change. The single best point gives you a beautiful result on one day and unpredictable outcomes everywhere else.
Pro Insight: A staged DOE approach with screening runs followed by response-surface refinement typically requires 25 to 50 boards for initial qualification, with confirmation runs on independent lots. This sounds like a lot, but it costs far less than six months of reactive troubleshooting and rework on a high-volume line.
Run confirmation boards at your proposed center and at two or three nearby points. If all three locations produce acceptable results, you’ve found a window. If only the exact center passes, your window is too narrow and needs adjustment before production release.
6. Diagnose Defects by Reading Parameter Interactions
When something goes wrong, most people start tweaking settings immediately. That’s the fastest way to make things worse. Here’s why: in selective soldering, defects almost never have a single cause. They’re the result of two or three parameters interacting in the wrong combination.
Build a Systematic Symptom-to-Cause Path
Before you touch any setting, collect evidence. That means thermal profiles, machine logs, visual inspection, and X-ray where you can get it. You need to know whether the problem is thermal, chemical, geometric, or mechanical.
For insufficient barrel fill or non-wetting, work through this checklist in order:
-
Check solderability first. Run a solderability test on the pad and lead finish. If the surfaces are oxidized or contaminated, no setting change will fix it.
-
Verify hole-to-lead geometry. Measure the clearance. Too tight and solder can’t flow. Too loose and there’s not enough capillary action.
-
Confirm flux coverage. Did the flux actually reach the joint? Is the flux jet aligned? Is the pattern correct for the hole size?
-
Assess thermal demand. Is there a copper plane pulling heat away? What’s the thermal mass of the joint compared to your calibration board?
-
Measure actual contact time. Calculate it from your path length and speed. Then verify with a thermal profile.
-
Check wave stability. Run the wettable coupon test. Is the wave consistent or oscillating?
-
Look for oxidation. Check your nitrogen settings and flux compatibility with your atmosphere.
Only after all seven steps should you start adjusting settings. And adjust one thing at a time.
Bridges, Icicles, and Solder Balls
These three defects share a common thread: too much solder in the wrong place. But the causes differ.
Bridges happen when solder connects adjacent pins. The usual suspects are: insufficient nozzle clearance from neighboring components, wave height too high for the pitch, immersion depth excessive, path direction running parallel to fine-pitch leads, poor peel-off at withdrawal, and flux spreading into areas it shouldn’t.
Icicles are elongated solder protrusions that form when solder doesn’t retract cleanly. Long lead protrusion, incorrect withdrawal angle, excessive solder temperature, and turbulence at the wave surface all contribute.
Solder balls are scattered spheres of solder on the board surface. These often come from thermal shock (board too cold hitting hot solder), flux containing moisture or solvents that flash-boil, excessive flux quantity splattering, and wave turbulence ejecting droplets.
Latent Reliability Risks
Here’s the uncomfortable part. Some defects look fine visually but cause field failures months later. Excessive intermetallic growth happens when contact time or temperature runs too high. The intermetallic layer at the pad-solder interface gets thick and brittle. You won’t see it without cross-sectioning.
Copper dissolution is similar. High pot temperature and long contact times eat into your annular rings over multiple assemblies. One board might pass inspection, but the copper is thinner than it should be.
Lifted pads, laminate damage, and component overheating are obvious reliability killers. But ionic residue is sneaky. A board can pass visual inspection and still fail in the field because flux residue absorbs moisture and creates leakage paths.
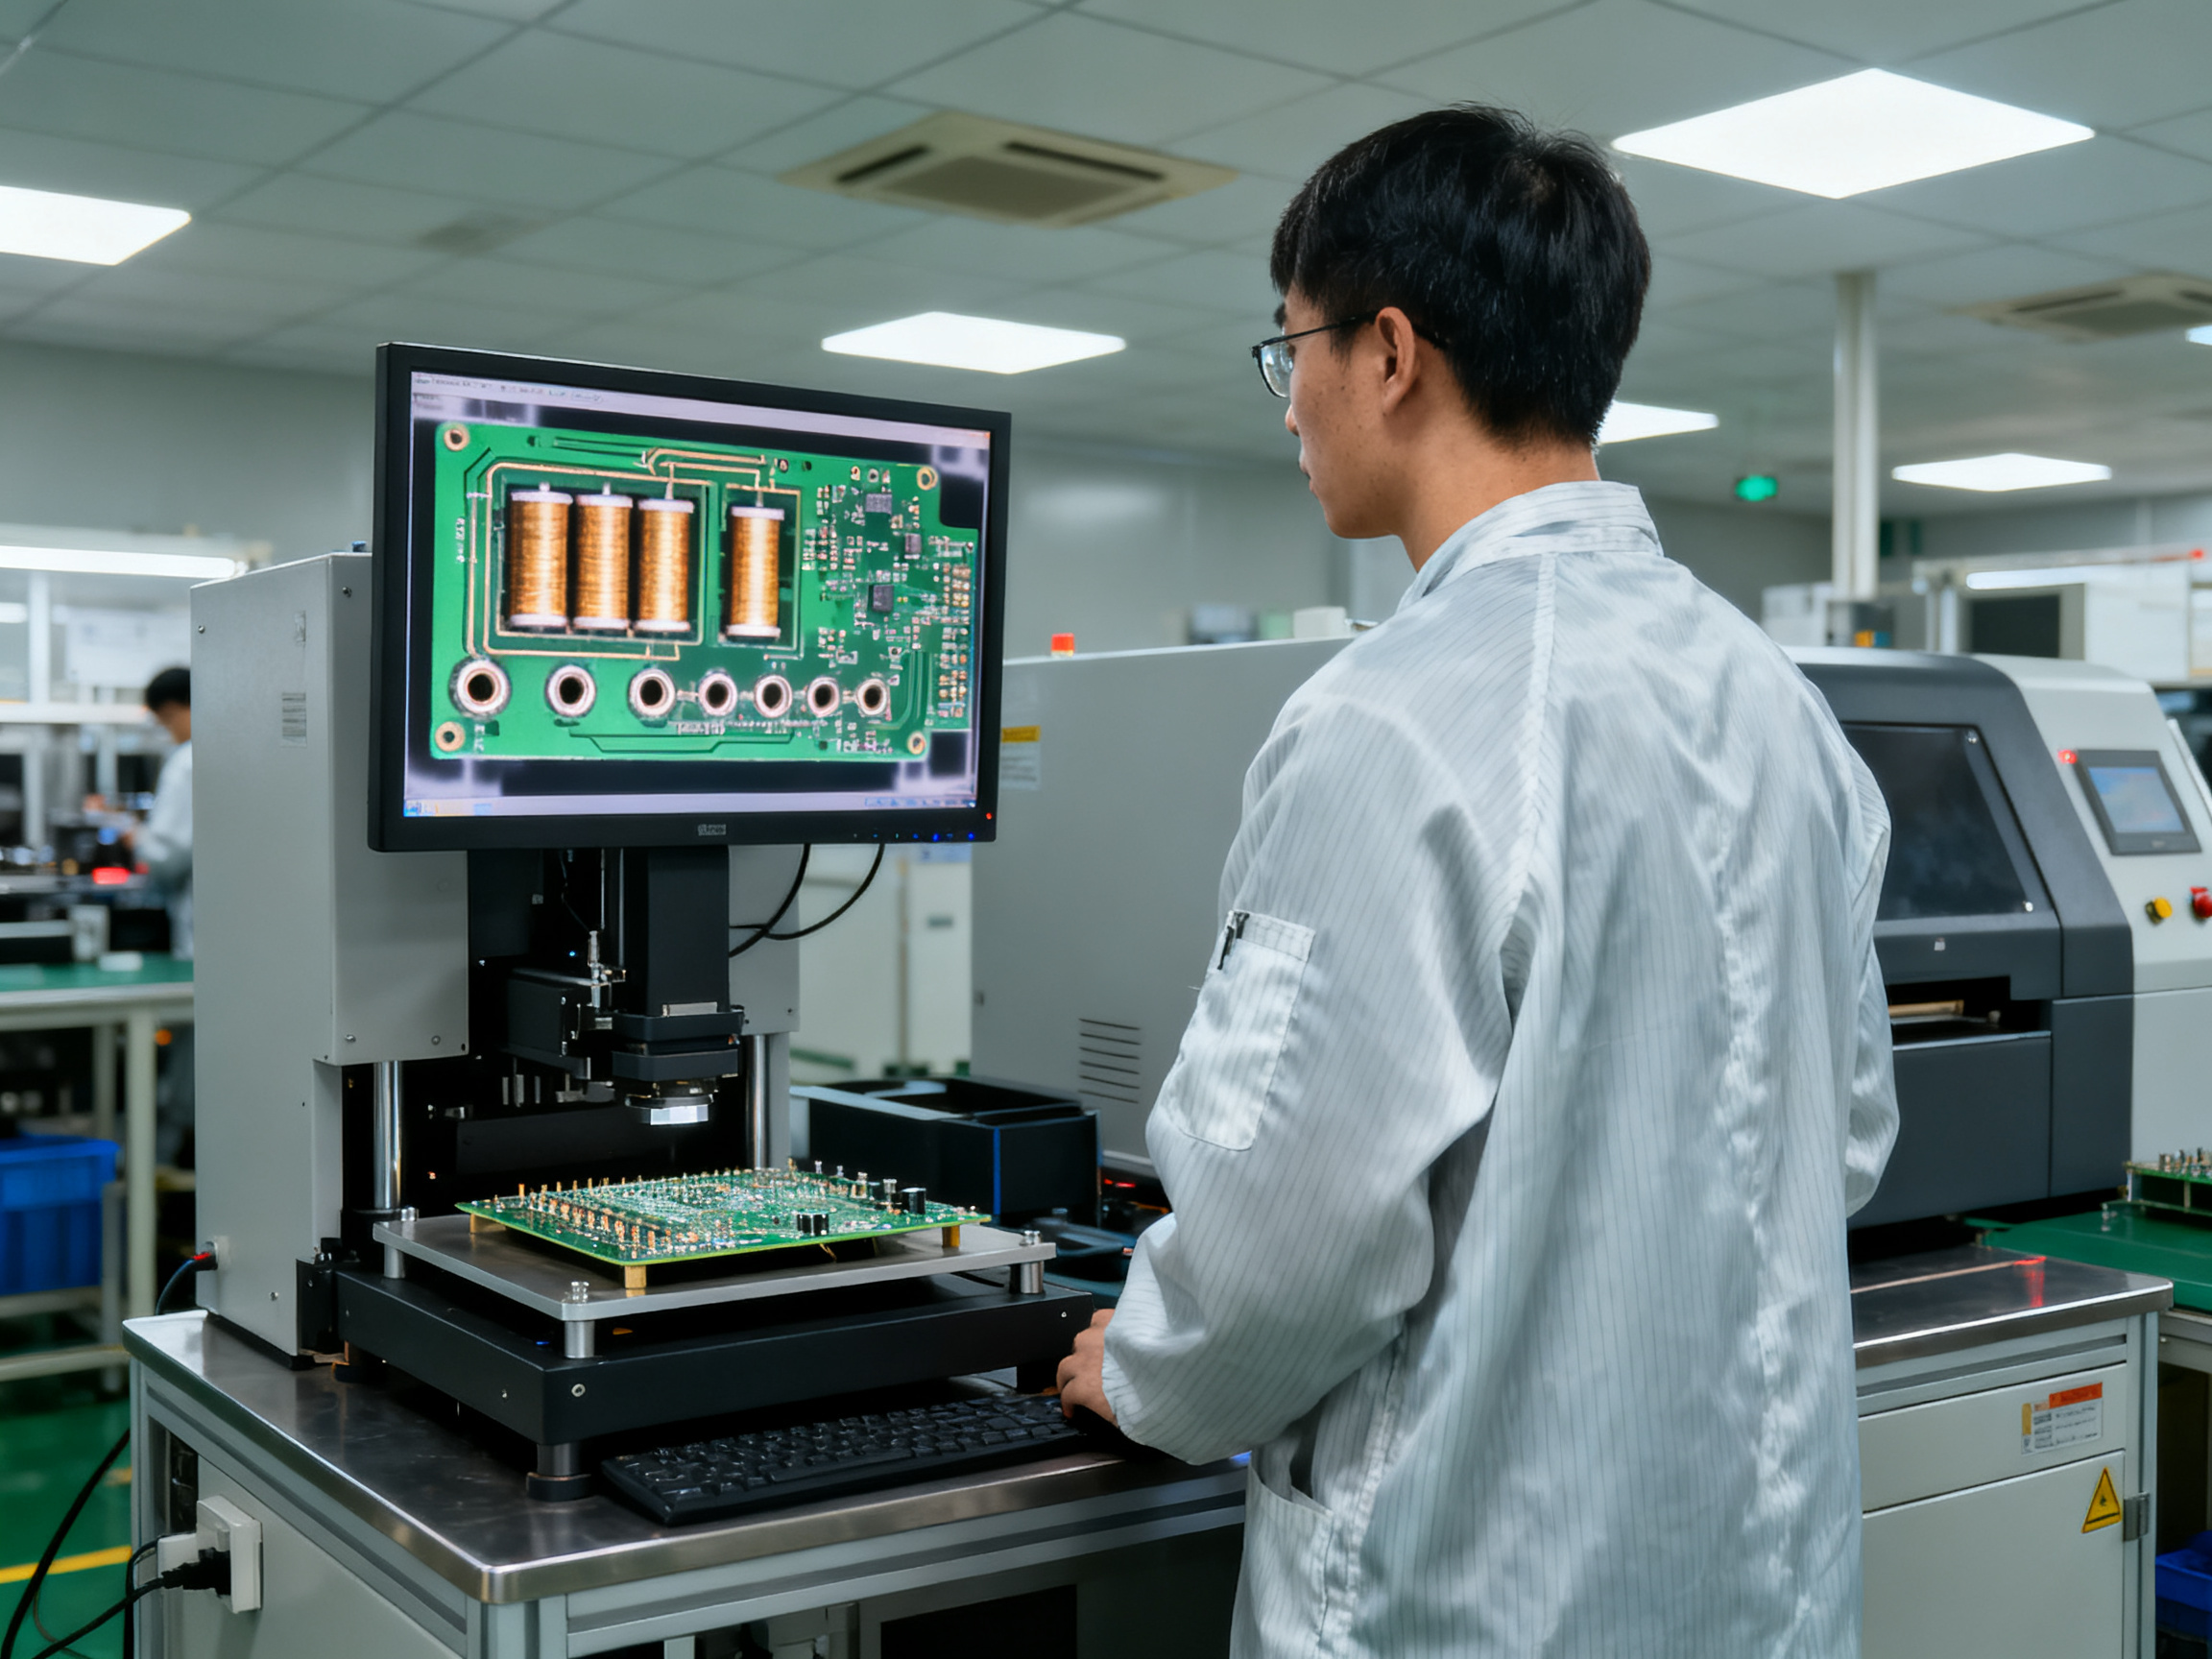
⚠️ Caution: Cross-sectioning, metallographic analysis, and ionic contamination testing require specialized equipment and training. Don’t attempt destructive analysis without proper facilities or qualified laboratory support.
Troubleshooting Quick Reference
| Symptom | Evidence to Collect | Likely Causes | Corrective Action |
|—|—|—|—|
| Insufficient fill | Thermal profile, X-ray, hole geometry | Low preheat, short dwell, high speed | Increase temperature, slow speed, verify flux |
| Bridges | AOI, dimensional check, path review | Wave too high, clearance too tight, flux spread | Reduce wave height, increase clearance, adjust flux |
| Icicles | Visual inspection, withdrawal review | Long leads, poor peel-off, high temp | Trim leads, adjust angle/speed, reduce temp |
| Solder balls | Flux review, preheat check, wave observation | Thermal shock, moisture, turbulence | Improve preheat, dry flux, stabilize wave |
| Non-wetting | Solderability test, flux activity, surface condition | Oxidation, contamination, insufficient heat | Clean or replace parts, verify flux, increase heat |
The key to good diagnostics is patience and systematic data collection. Jump to conclusions and you’ll spend weeks chasing shadows.
7. Lock, Monitor, and Transfer the Validated Recipe
Now that you have a validated process window from your DOE work, it is time to treat that recipe like a controlled asset, not just a machine file. This is where most shops fall apart. They optimize a great recipe, put it into production, and then watch it slowly drift because nobody locked it down or watched the right signals.
What goes into a locked recipe
Your approved recipe needs to be a complete package, not just a settings file. It should include product revision and machine identity, nozzle type and serial number, alloy and flux specifications with lot numbers and expiry dates, the complete solder path with all parameter tolerances, thermal profile evidence from your qualification boards, the inspection plan that defines what gets checked and how, software and firmware version, and any authorized change controls. Without all of these pieces, you do not have traceability when something goes wrong six months from now.
What to monitor in production
Track your leading indicators every shift or every batch. Pot temperature and solder level, wave height stability, nozzle condition, flux deposition quantity and pattern, nitrogen flow and oxygen concentration, preheat output temperatures, actual board temperature at key points, and consumable lot numbers alongside your yield and defect trends. These signals tell you something is drifting before you get a board full of bad joints.
Control limits and reaction plans
Set your control limits from what your process actually demonstrated during qualification, not from equipment manufacturer ranges. When something drifts outside those limits, you need a defined reaction plan. Some changes require full requalification. Others just need a few confirmation boards. The difference matters because requalification takes time and money.
| Parameter | Baseline value | Validated range | Control limit | Alarm threshold | Reaction plan |
|—|—|—|—|—|—|
| Pot temperature | 260°C | 255 to 265°C | +/-5°C | +/-7°C | Check thermocouple, verify calibration |
| Contact time | 3.0s | 2.5 to 3.5s | +/-0.5s | +/-0.8s | Verify speed, check path length |
| Flux volume | 0.8mL | 0.6 to 1.0mL | +/-0.2mL | +/-0.3mL | Inspect jet, check pressure settings |
| Oxygen level | 200ppm | 100 to 300ppm | +/-50ppm | +/-100ppm | Check nitrogen supply, inspect seals |
The change-trigger matrix
Not every change needs the same response. A new PCB revision or flux chemistry probably needs full requalification. A like-for-like nozzle swap might only need a few confirmation boards. A software patch needs an impact assessment first. Define these categories before you need them, not during a crisis.
The real answer to how you know your selective soldering process settings are right is this: you lock the validated window, you monitor the signals that predict trouble, and you control changes with discipline. That is not a perfect recipe sitting in a spreadsheet somewhere. That is a living process you can trust.
Conclusion: Use a Measured Process Window, Not a Universal Recipe
The selective soldering workflow comes down to five steps: define your product constraints and acceptance criteria, calculate a defensible baseline from manufacturer data, profile the actual assembly under real conditions, run designed experiments to find the true optimum, and then lock the window with SPC and change control.
The recommendation here is straightforward. Before you raise the pot temperature or extend dwell time to fix a fill problem, verify that your thermal profile and solder wave are actually behaving as expected. Add heat to a process that already has hidden instability, and you’ll create new problems while solving old ones.
From Our Experience: Processes that appear stable on paper can hide problems like solder level drift, flux jet misalignment, or nitrogen distribution gaps. Physical verification before adjustment catches these issues quickly and prevents over-correction.
Five-Step Implementation Summary
- Define product requirements, material specs, and acceptance criteria
- Calculate baseline parameters from manufacturer limits and process equations
- Profile the real assembly with thermocouples and physical wave verification
- Optimize through DOE to find the centered, robust process window
- Lock and monitor with SPC, calibration traceability, and change control
Next Steps by Role
| Role | Immediate Action | Long-Term Goal |
|—|—|—|
| Production leader | Review current recipe documentation for traceability gaps | Implement shift-by-shift monitoring dashboards |
| Process engineer | Run physical wave verification on next setup | Establish DOE capability for new product introductions |
| Procurement | Audit material specifications against baseline limits | Qualify alternate suppliers with documented process impact |
| Technology officer | Assess equipment data logging and SPC integration | Plan upgrade path for recipe management and monitoring systems |
The companies that get consistent selective soldering results in 2026 are the ones who stopped looking for magic recipes. They built the workflow instead.