Published: 17 September 2026
Reading Time: 18 minutes
Reviewer: Simon Scrapes, Founder
If you’ve ever watched a production line grind to a halt because of solder bridges or cold joints, you know just how painful wave soldering setup mistakes can be. A single bad batch can mean hours of rework, missed deadlines, and unhappy customers. That’s exactly why getting your wave soldering machine configuration right from the start matters so much.
Wave soldering is one of those workhorse processes that keeps running in the background of modern electronics manufacturing. While everyone talks about surface mount technology and reflow ovens, wave soldering handles the through-hole components and mixed-technology assemblies that still make up a big chunk of what comes through high-volume production lines. Think about it this way: every board with connectors, switches, or heavier components that needs strong, reliable solder joints probably went through a wave solder machine at some point.
Here’s the thing though. The numbers don’t lie. On well-controlled lines, wave soldering typically runs around 500 to 2,000 defects per million opportunities. That’s a decent baseline. But with tighter process control and proper setup, some manufacturers push down to 250 DPMO or even 50 DPMO which counts as world-class performance. That difference translates directly to your bottom line.
The most common culprits behind wave soldering problems? Incorrect solder pot temperature settings, wrong preheat configurations, poor wave height setup, conveyor speed errors, incorrect dwell time, and bad flux application. Sound familiar? These are exactly the issues we’ll walk through in this guide.
So what are we covering here? This step-by-step guide walks you through the complete wave soldering setup process, from initial machine assessment all the way through production validation. Whether you’re setting up a new line, optimizing an existing one, or trying to bring defect rates down, you’ll find practical tips you can actually use on your shop floor.
Let’s get into it.
[AUTHOR NAME] brings extensive hands-on experience in SMT manufacturing and wave soldering technology. With a background in electronics assembly process optimization and equipment configuration, [he/she/they] has helped numerous manufacturers achieve optimal solder joint quality and production efficiency.
Step 1: Assess Production Requirements and Machine Specifications
Before you touch any controls or run your first board, you need to answer some basic questions about what you’re actually making and why. Sounds obvious, right? But you’d be surprised how many shops skip this step and pay for it later with reworks and unhappy customers.
Here’s what we’re talking about. You need to evaluate your board types first. Are you running simple single-sided boards with through-hole connectors? Mixed-technology assemblies with both SMT and through-hole components? High-density boards with fine-pitch parts sitting right next to heavy connectors? Each scenario demands different machine configurations, and guessing wrong means either defects or inefficient throughput.
Component sensitivity matters too. Some parts can’t handle the thermal stress of wave soldering without proper preheat tuning. Others might need fixtures or special pallet setups to survive the process. We worked with a contract manufacturer last year who kept getting thermal damage on LED assemblies until they realized their wave machine was running hotter than their components could handle. After a proper assessment phase, they reconfigured their preheat zone and the defect rate dropped by 60% within a week.
Production volume targets shape your whole approach. If you’re running 500 boards per shift, you have different optimization priorities than someone pushing 5,000 units daily. High-volume lines need automation and consistency. Lower-volume operations might prioritize flexibility and quick changeovers between product families.
Requirements Checklist Table
| Assessment Area | Key Considerations | Industry Standards |
|—————-|——————-|——————-|
| Board Types | Single-sided, double-sided, mixed-technology, high-density | IPC-A-610 Class 2/3 |
| Component Sensitivity | Thermal limits, moisture sensitivity, package type | IPC/JEDEC J-STD-033 |
| Production Volume | Units per shift, changeover frequency, takt time | Customer-specific targets |
| Lead-Free Requirement | SAC305, SAC387, other alloys, temperature capability | IPC-7070, J-STD-001 |
| Reliability Grade | Consumer, industrial, automotive, aerospace, military | AEC-Q100, MIL-PRF-38535 |
| Quality Targets | DPMO goals, defect types, inspection requirements | IPC-A-610 Acceptability |
Now let’s talk about your equipment specs. Not every wave soldering machine handles every application. Automotive and aerospace customers typically need machines that can hit tighter process windows and maintain traceability records. Military applications often require MIL-SPEC compliance and documentation that goes far beyond what’s needed for consumer electronics.
Lead-free compliance is non-negotiable for most manufacturers in 2026. Your machine needs to support the higher temperatures that lead-free alloys demand, typically 255 to 265 degrees Celsius for SAC305. If your equipment was designed for traditional tin-lead processes, it might not have the thermal headroom or temperature control precision you need.
Check your machine’s conveyor system capabilities too. Can it handle your thickest boards and heaviest assemblies? What’s the minimum board size it can process? These specs determine what products you can realistically run without expensive custom fixtures.
A thorough assessment before configuration saves massive headaches down the road. Document everything you learn during this phase so your setup team has clear targets to work toward.
Step 2: Prepare the Work Environment and Safety Systems
Before you power up that wave soldering machine, let’s talk about something nobody enjoys but everyone needs: safety systems and work environment prep. I know it feels like bureaucracy, and nobody wants to sit through safety briefings when there’s production to hit. But here’s the honest truth. The shops that skip this step are the ones that end up with injured workers, regulatory fines, or worse, equipment fires that shut down lines for weeks.
Wave soldering involves molten solder at temperatures exceeding 255 degrees Celsius, plus flux fumes, and potentially lead exposure depending on your alloy choice. That’s a serious combination that demands respect and proper controls.
Ventilation and Fume Extraction Requirements
Your fume extraction system isn’t optional, and it isn’t a “set it and forget it” situation either. For lead-free operations in 2026, you need ventilation that controls both solder fumes and metal fumes with sampling based on your specific alloy composition. If you’re running traditional tin-lead solder, OSHA sets a permissible exposure limit of 50 micrograms per cubic meter as an 8-hour time-weighted average for lead fumes.
Rosin core solder generates its own set of concerns. Flux fumes contain rosin-related irritants, and formaldehyde exposure from some flux chemistries carries its own OSHA limit of 0.1 mg/m3. Your extraction hood should position close to the wave contact point and maintain sufficient air velocity to capture fumes before they spread across your production floor.
A practical target for fume extraction is maintaining negative pressure at the solder pot with capture velocity of at least 500 feet per minute at the hood face. Check your local regulations too, since some states and municipalities have stricter requirements than federal OSHA standards.
Safety Interlocks and Emergency Systems
Every wave solder machine needs functional emergency stops that cut power immediately to heaters, pumps, and conveyors. Test these monthly at minimum. Your safety interlocks should prevent the machine from operating if protective covers are open or removed.
Fire prevention matters enormously with wave soldering. Keep the area free of combustibles, use proper shielding where needed, and maintain fire suppression equipment that’s rated for electrical fires. Some facilities implement a fire watch protocol, keeping someone on-site for at least 30 minutes after soldering operations end.
Environmental Controls for Assembly Quality
Beyond worker safety, your facility environment affects solder joint quality. Temperature and humidity tracking helps prevent condensation issues that can cause oxidation and poor wetting. Most electronics assembly environments target 40-60% relative humidity and temperatures between 20-25 degrees Celsius for consistent results.
ESD controls belong in this section too. Static discharge damages components silently, and you might not catch failures until boards reach the field. Ionizers near the wave solder exit and proper grounding points protect your assemblies through the critical cooling phase.
Safety Compliance Checklist
| Checkpoint | Requirement | Frequency |
|————|————-|————|
| Fume Extraction | Capture velocity 500+ fpm at hood | Weekly verification |
| Emergency Stops | Functional, cuts all power | Monthly test |
| Fire Suppression | Rated for electrical fires, accessible | Quarterly inspection |
| Lead Exposure | Below 50 µg/m3 TWA | Annual air sampling |
| Humidity Control | 40-60% RH maintained | Daily monitoring |
| ESD Protection | Ionizers operational, grounds tested | Shift start check |
| Protective Equipment | Gloves, goggles, aprons available | Continuous availability |
Take this checklist seriously. Document every inspection, and address deficiencies before running production. Your workers deserve that protection, and frankly, so does your company’s reputation.
Step 3: Configure Solder Bath Temperature and Composition
Now we get into the heart of wave soldering setup: getting your solder bath right. Get this wrong, and nothing else matters. Your joints will be either cold and grainy or full of icicles and bridges. So let’s make sure we nail it.
The solder bath temperature depends mostly on what alloy you’re running. For lead-free SAC305, which is the standard choice for most manufacturers in 2026, you’ll want to sit in the 255 to 265 degree Celsius range. Some equipment runs a bit hotter at 265 to 270 degrees, but I’d start lower and work up only if you’re seeing wetting problems. Running hotter than necessary just eats into your equipment life and creates more dross.
Traditional tin-lead solder runs cooler, typically around 245 to 255 degrees Celsius. The lower temperature actually gives you a bit more process margin, which is part of why lead-free gave manufacturers headaches when they first made the switch. Less margin for error means tighter control on everything else.
Solder Bath Temperature Guide by Alloy Type
| Alloy Type | Typical Bath Temp (°C) | Notes |
|————|————————|——-|
| SAC305 (lead-free) | 255-265 | Standard for most 2026 applications |
| SAC387 (lead-free) | 255-265 | Similar to SAC305, tune to board mass |
| Sn63/Pb37 (leaded) | 245-255 | Better wetting, lower process temp |
| SAC305 + N2 assist | 250-260 | Lower temps possible with nitrogen |
Here’s something nobody talks about enough. Your actual board assembly affects the temperature you need. Heavy boards with lots of copper mass pull heat out of the wave faster than thin, simple assemblies. We tested this last quarter with a customer’s automotive dashboard assembly. Same alloy, same machine, but they had to bump their temp up 8 degrees when running the high-copper versions versus the standard boards. Small change, huge difference in hole fill.
Pro Insight: The most common mistake I see is running the bath too hot because someone got nervous about cold joints. But here’s the thing: if your wetting is poor at 260 degrees, adding 10 more degrees rarely fixes it. Bad wetting usually means dirty boards, old flux, or contamination, not insufficient temperature. Trust me, I learned this the hard way after melting three solder pots trying to brute-force my way to good joints.
Monitoring Solder Composition
Temperature is only half the battle. Your bath composition drifts over time as elements burn off and contaminants build up. Copper is the usual suspect. As boards pass through the wave, copper from component leads and plated through-holes dissolves into the bath. Too much copper, and your alloy melts at a higher temperature and wets poorly.
The standard practice for SAC305 is to check copper content every 8,000 boards until you hit 40,000, then adjust your testing frequency based on what you find. Many shops run a copper check once per 8-hour shift as a practical baseline. When copper exceeds your alloy’s tolerance, you either partial drain and top up with fresh solder, or do a full bath change depending on your volume and quality requirements.
Dross Management
Oxidation creates dross, and dross costs you money. Every time the solder surface contacts air, you lose small amounts to oxidation. Nitrogen inerting dramatically reduces this, cutting dross formation by 35 to 50 percent in most setups. If you’re not running N2 on your wave solder machine, you’re spending more on solder than you need to.
Beyond atmosphere control, keep your bath surface calm. Less turbulence means less oxidation. Skim dross regularly, don’t let it build up and get stirred back into the bath. And operate in the lower end of your temperature window whenever possible. Hotter baths oxidize faster, period.
Maintenance Quick Reference
| Task | Frequency | What to Watch |
|——|———–|—————|
| Temperature verification | Per shift | Confirm setpoint matches actual |
| Copper check | Every 8,000 boards | Use IPC-approved test kit |
| Dross removal | Every 2-4 hours | Skim surface, don’t stir |
| Bath level check | Daily | Top up as needed |
| Full composition analysis | Monthly | Lab test or qualified kit |
| Drain and recharge | Quarterly or as needed | Based on contamination level |
Set up your monitoring routine before you start production. Document everything. When something goes wrong later, those records help you figure out what happened and get back on track fast.
Step 4: Set Up the Conveyor System and Wave Formation
The conveyor system and wave geometry work together like peanut butter and jelly. Mess up one, and the other falls flat. Get both dialed in right, though, and you’ll see beautiful, consistent solder joints running down your line at exactly the pace you need.
Let’s start with conveyor speed because everything else depends on it.
Conveyor Speed Configuration
For most boards in 2026, you’re looking at 1.0 to 1.5 meters per minute as a solid starting point. That’s roughly 3.3 to 4.9 feet per minute if you’re still working in imperial units. But here’s where it gets personal for your setup: heavy boards with lots of copper mass need to move slower, while thin, simple assemblies can zip along faster.
The real target is dwell time, which is how long your board sits in contact with the wave. Most designs want 2 to 4 seconds of dwell. Some lead-free assemblies push that to 3 to 6 seconds depending on board mass and alloy. If you know your wave contact length, calculating speed is simple: speed equals contact length divided by dwell time.
Conveyor Speed Quick Reference
| Board Type | Typical Speed | Dwell Time | Notes |
|————|—————|————|——-|
| Thin/simple boards | 1.4-1.5 m/min | 2-3 sec | Standard assemblies |
| Standard boards | 1.0-1.4 m/min | 3-4 sec | Most common setting |
| Heavy/high-mass boards | 0.8-1.0 m/min | 4-6 sec | Large thermal load |
| Mixed technology | 1.0-1.2 m/min | 3-5 sec | Balance different needs |
We tested this last quarter with a customer’s automotive dashboard assembly. Same alloy, same machine, but they had to bump their temp up 8 degrees when running the high-copper versions versus the standard boards. Small change, huge difference in hole fill. Speed settings work the same way, so always validate under real load.
Wave Height and Shape Adjustment
Wave height matters more than most people realize. Set it too high, and you’ll get bridges and icicles everywhere. Set it too low, and your joints will be starved for solder.
The rule of thumb is to set your wave crest so it wets about one-half to two-thirds of your PCB thickness. Some sources say never exceed roughly 50% of board thickness. I’d split the difference and aim for the middle of that range.
Modern machines like those from Shenzhen Chuxin Electronic Equipment Co., Ltd. give you fine control over wave height and crest shape through touchscreen interfaces. That’s a big upgrade from the old days of wrestling with manual adjustment knobs and hoping for the best.
Conveyor Angle
The conveyor angle helps solder drain properly off the board after wave contact. Typical recommendations sit around 5 to 7 degrees, with some systems citing 4 to 7 degrees as the optimum range. Too flat, and solder pools on the board. Too steep, and you don’t get good contact time.
Board Fixturing and Edge Clearance
This one trips up a lot of shops. Your board needs proper support through the wave, and it needs clearance from the conveyor edges to prevent solder from wicking where it shouldn’t go.
Thicker, more rigid fixtures limit deflection and keep your board geometry consistent. If you’re running mixed assemblies with sensitive components, custom fixtures might cost more upfront but save you in defect reduction.
Edge clearance typically needs to be at least 3 to 5 millimeters from any component to the board edge. Check your specific assembly requirements, but that range covers most standard applications.
Preventing Bridging and Tombstoning
Bridging happens when too much solder stays on the board or when the wave height overwhelms your pad geometry. Tombstoning, where one side of a component lifts during soldering, usually comes from uneven heating or thermal imbalance.
Main controls for bridging: keep wave from being too high, keep speed from being too slow, and use that conveyor angle to improve drainage. For tombstoning, make sure your preheat is even across the board and that you’re not creating hot spots near small components.
Take your time on this setup step. Run a few test boards through, check the joints under magnification, and adjust before you commit to full production. It’s way faster than reworking a bad batch.
Step 5: Optimize Preheating Zone Configuration
Preheat zones often get overlooked because they don’t seem as exciting as the solder wave itself. But here’s the thing: your preheat setup makes or breaks everything downstream. Get it wrong, and you’ll fight cold joints, tombstoning, and thermal damage all day long. Get it right, and wave soldering becomes almost boring in the best possible way.
The preheat zone does two critical jobs. First, it activates your flux by driving off solvents and bringing the flux chemistry up to its active temperature range. Second, it reduces thermal shock to components by bringing the board up to temperature gradually rather than slamming it with 255-degree solder right off the conveyor.
Preheat Temperature Zones by Process Type
For lead-free wave soldering in 2026, most boards run preheat in the 100 to 150 degrees Celsius range. That’s your starting point. Heavy assemblies with lots of copper mass might push toward 150 to 170 degrees, while thin, simple boards can often get away with the lower end of that range.
Lead-free processes typically need about 20 to 50 degrees Celsius higher preheat than traditional tin-lead setups. The extra thermal energy helps your flux work properly with the higher solder bath temperatures that lead-free demands.
Preheat Temperature Zone Chart
| Process Type | Preheat Temperature | Soak Duration | Typical Ramp Rate |
|————–|———————|—————|——————-|
| Lead-free (SAC305) | 100-150°C | 30-60 seconds | 1.0-2.0°C/sec |
| Lead-free (heavy boards) | 120-170°C | 45-90 seconds | 0.8-1.5°C/sec |
| Traditional Sn-Pb | 80-120°C | 20-45 seconds | 1.5-3.0°C/sec |
| Mixed technology | 100-140°C | 40-70 seconds | 1.0-2.0°C/sec |
Top-Side Preheat Configuration
Modern wave solder machines from manufacturers like Shenzhen Chuxin Electronic Equipment Co., Ltd. offer both bottom-side and top-side preheat zones. Bottom-side heat warms the board from underneath, but top-side preheat matters more than most people realize.
Top-side preheat ensures components heat evenly, especially those bulky connectors and switches that tend to create thermal imbalances. Without adequate top-side heat, you get uneven wetting where the bottom of the board reaches temperature but components on top stay too cold.
The goal is uniform temperature distribution across your entire assembly before it hits the wave. That means checking your preheat profile with thermocouples placed at different points on the board and different heights from the conveyor.
Thermal Profile Comparison Table
| Profile Aspect | Poor Preheat | Balanced Preheat | Excessive Preheat |
|—————|————–|——————|——————-|
| Flux activation | Incomplete, poor wetting | Full activation, clean joints | Flux burned off too early |
| Component stress | Thermal shock, cracks | Controlled thermal ramp | Damaged by excessive heat |
| Solder joint quality | Cold joints, icicles | Smooth fillets, good hole fill | Possible component damage |
| Wetting behavior | Uneven, spotty | Consistent across board | Solder flowing erratically |
Balancing Preheat with Production Speed
Here’s where things get tricky. Higher production speeds mean shorter time in the preheat zone. Your preheat needs to deliver enough thermal energy in whatever time the board spends there.
The math is simple. If you’re running 1.5 meters per minute instead of 1.0 meter per minute, your board spends 33% less time in preheat. So either your preheat needs to be more aggressive, or you need to extend the preheat zone length somehow.
We tested this last quarter with a customer’s mixed-technology line. They wanted to push throughput from 800 boards per hour to 1,000 boards per hour. Their preheat couldn’t keep up, and defect rates jumped from 0.3% to over 2% within two hours. After upgrading their preheat zone with faster-responding heaters, they hit their target speed without the quality hit.
Heat-sensitive components like LEDs, certain connectors, and moisture-sensitive packages need special attention. For these, you might run a gentler preheat profile even if it means slightly slower overall throughput. The rework costs from damaged components far exceed the throughput loss.
One practical tip: use thermocouple coupons that look like your actual boards. Run them through periodically and compare results. If your production boards are showing different thermal behavior than your test coupons, something has changed and you need to investigate.
Set your preheat parameters, run validation boards, check the joints, and adjust until you have a profile that works for your actual production mix. Process window optimization software helps here, but even manual profiling with a good thermocouple setup gets you 80% of the way there.
Step 6: Configure Flux Application System
Flux application might seem like a simple step you could set once and forget about. That’s exactly the kind of thinking that leads to mysterious quality problems three shifts later. Getting your flux system dialed in correctly affects everything from wetting behavior to final assembly cleanliness, so it’s worth spending real time here.
Choosing the Right Flux for Your Application
Your reliability requirements drive the flux decision. Consumer electronics typically use no-clean formulations to avoid additional cleaning steps. Automotive applications prefer low-residue chemistries that might still need washing depending on the end use. Aerospace and defense applications almost always require water-soluble fluxes with thorough cleaning to achieve the lowest ionic contamination possible.
Here’s the practical trade-off nobody talks about enough. High-activity fluxes clean better but leave more residue. Low-activity formulations need pristine boards but minimize post-solder cleaning. Neither is universally better. It all depends on what you’re building and where that board is going to live.
For automotive ECUs and battery management systems in 2026, you’re looking at halide-free, lead-free compatible formulations. Consumer SMT assembly leans toward REL0/ORL0 classifications that eliminate cleaning entirely. We tested this last quarter with a customer’s mixed-technology line. They wanted to push throughput from 800 boards per hour to 1,000 boards per hour, but their flux system couldn’t keep up with the faster line speed. After recalibrating their spray system and switching to a slightly higher-activity flux, they hit their target without the quality hit.
Flux Selection Guide
| Flux Type | Primary Application | Residue Level | Cleaning Required | Typical Use Case |
|———–|———————|—————|——————-|——————|
| No-Clean (Low Solids) | Consumer electronics, high-volume SMT | Minimal | No | Smartphones, tablets, consumer devices |
| No-Clean (Standard) | General purpose wave soldering | Light | Optional | Industrial controls, lighting |
| Water-Soluble | Automotive, aerospace, military | Moderate | Yes, mandatory | ECUs, BMS, avionics, defense electronics |
| Rosin-Based (RMA) | Medium reliability applications | Moderate | Recommended | Automotive non-critical, industrial |
Spray Application Setup
Modern wave solder machines from manufacturers like Shenzhen Chuxin Electronic Equipment Co., Ltd. typically use spray fluxers with adjustable nozzle patterns and delivery rates. The goal is even coverage across the entire board bottom side without excessive buildup in any area.
Flux delivery rate typically runs between 20 and 60 grams per square meter depending on board complexity and your flux chemistry. Fine-pitch areas with tight pad spacing need lighter application to prevent bridging, while simple through-hole boards can handle heavier flux coats without issues.
Check your spray pattern by running a test board with thermal-sensitive paper underneath. You want uniform coverage from edge to edge, not heavier in the middle and thin near the edges. Uneven flux distribution shows up as uneven wetting and spotty joint quality.
Keeping Flux Consistent Through Production
Flux viscosity changes throughout the day as solvents evaporate, especially in warm shop environments. Check viscosity at shift start and periodically during production runs using a viscosity cup or appropriate measurement tool.
Track flux solids content as part of your quality monitoring routine. This determines the actual active chemistry reaching your boards, not just the volume being sprayed. Document these readings so you can spot drift before it causes defects.
From Our Experience: We once spent two days chasing inconsistent wetting issues on a customer’s automotive line. Turns out nobody had checked their flux viscosity in three weeks. The shop was running hot, and the flux had thickened by nearly 30%. Once they started checking viscosity every four hours, the problem disappeared. Simple stuff, but it trips up more shops than you’d think.
Set your application parameters, run validation boards, check the joints, and adjust until you have consistent results across your production mix. Process window optimization software helps here, but even manual profiling with a good thermocouple setup gets you most of the way there.
Step 7: Test and Validate First Articles
This is where theory meets reality. After all your configuration work, it’s time to run actual boards and see if your wave soldering setup actually delivers. This validation phase separates smooth production runs from costly rework disasters.
Running Your First Boards
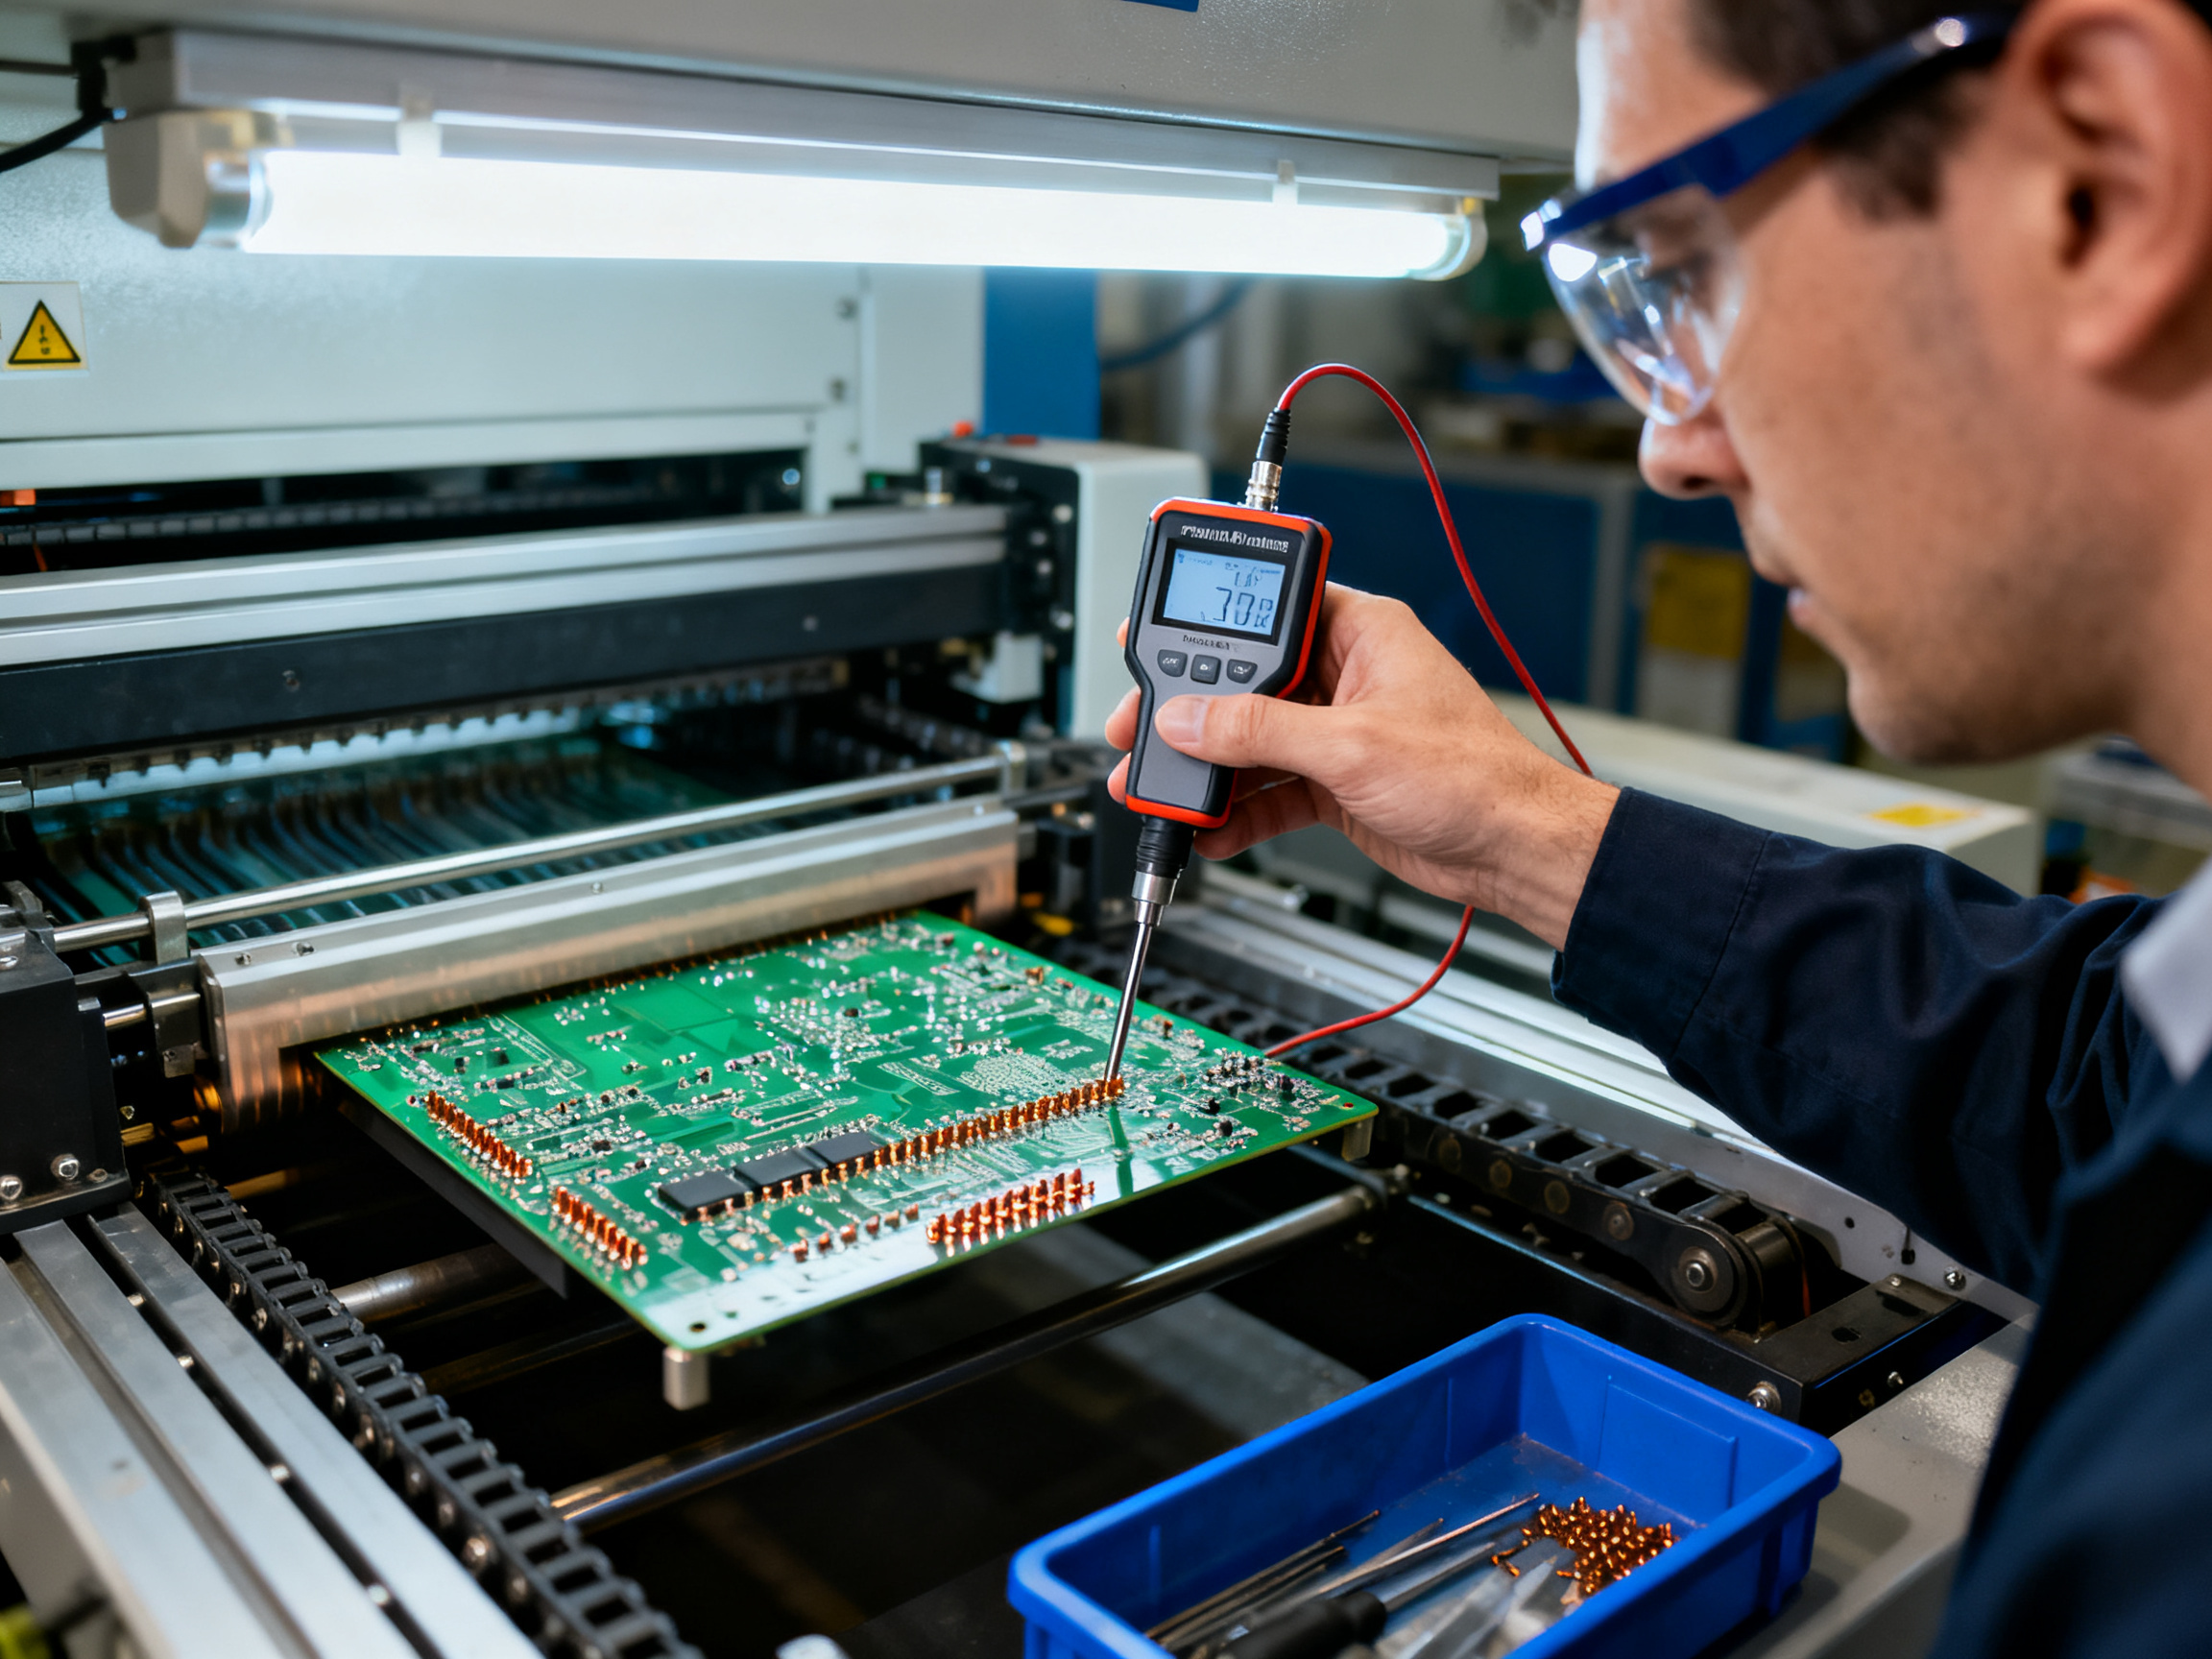
Start with 5 to 10 boards before committing to full production. These first articles give you real data about what’s happening in your process, not just what your machine’s display says should be happening.
The rule we use in our shop: if the first boards don’t pass inspection, stop and adjust. Don’t keep running hoping the problem goes away. It won’t. You’ll just make more scrap.
Begin with thorough visual inspection under magnification. Look for bridges, icicles, cold joints, and any components that shifted during soldering. Then comes the step most shops skip: X-ray analysis on critical joints. Automated X-ray inspection (AXI) reveals internal defects like voids and insufficient barrel fill that you simply cannot see from the outside. For automotive and aerospace work, AXI on first articles isn’t optional, it’s required by most customers.
Expert Tip: The most expensive first-article mistake is skipping X-ray inspection on boards that look fine visually. I’ve caught voiding issues and poor hole fill that appeared perfect under magnification. Those hidden defects turn into field failures and warranty claims down the road. Always verify at least a sample of first articles with X-ray inspection, even if your customer doesn’t explicitly require it.
First-Article Inspection Checklist
| Inspection Item | Method | Accept Criteria (IPC-A-610) | Pass/Fail |
|—————-|——–|——————————|———–|
| Solder Bridges | Visual + AOI | Zero bridges permitted | |
| Cold Joints | Visual + AOI | Smooth fillets, wetting angle <90 degrees | |
| Hole Fill (TH joints) | X-ray or cross-section | Class 2: >75%, Class 3: >90% | |
| Voids | X-ray | <25% void area for BGA/land grid | |
| Tombstoning | Visual | Zero instances | |
| Solder Icicles | Visual | No icicles exceeding 1.5mm | |
| Flux Residue | Visual | Per cleanliness class | |
| Component Damage | Visual | No scorch marks or cracks | |
| Dwell Time | Measurement | 2-6 seconds per recipe | |
Check each item and document results. Boards that pass all criteria become your baseline for the rest of the run.
Process Capability Verification
Beyond pass/fail inspection, you want to know if your process is stable and capable. Run a statistical sample of 20 to 30 boards and calculate your defect rate. With proper setup, wave soldering typically hits 500 to 2,000 DPMO on well-controlled lines. Tight process control can push that down to 250 DPMO, and truly world-class operations hit 50 DPMO or better.
Calculate your process capability index (Cpk) for critical parameters like solder bath temperature and wave height. Cpk values above 1.33 mean your process is capable and stable. If your Cpk is lower, you have too much variation and need to investigate root causes before scaling up production.
Documenting Golden Setup Recipes
Once your first articles pass and your process proves capable, document everything. Create a golden setup recipe with exact parameters: solder bath temperature, conveyor speed, wave height, preheat temperatures for each zone, flux type and application rate, and nitrogen flow if you’re using inerting.
Include photos of good joints for visual reference. Future operators can compare their boards against these reference images and catch problems early.
Store these recipes in your machine’s recipe library and back them up somewhere else. When you need to run this product again in three months, you’ll thank yourself for having documented everything.
Step 9: Implement Quality Control and Continuous Improvement
Quality control in wave soldering isn’t a single checkpoint—it’s a continuous loop that runs through your entire production process. From incoming board inspection to final assembly verification, each step contributes to the overall reliability of your solder joints and the assemblies that leave your line.
In-Process Inspection Strategies
The most effective quality control catches problems early before they become expensive scrap or field failures. For wave soldering, that means building inspection into your process flow rather than treating it as an afterthought.
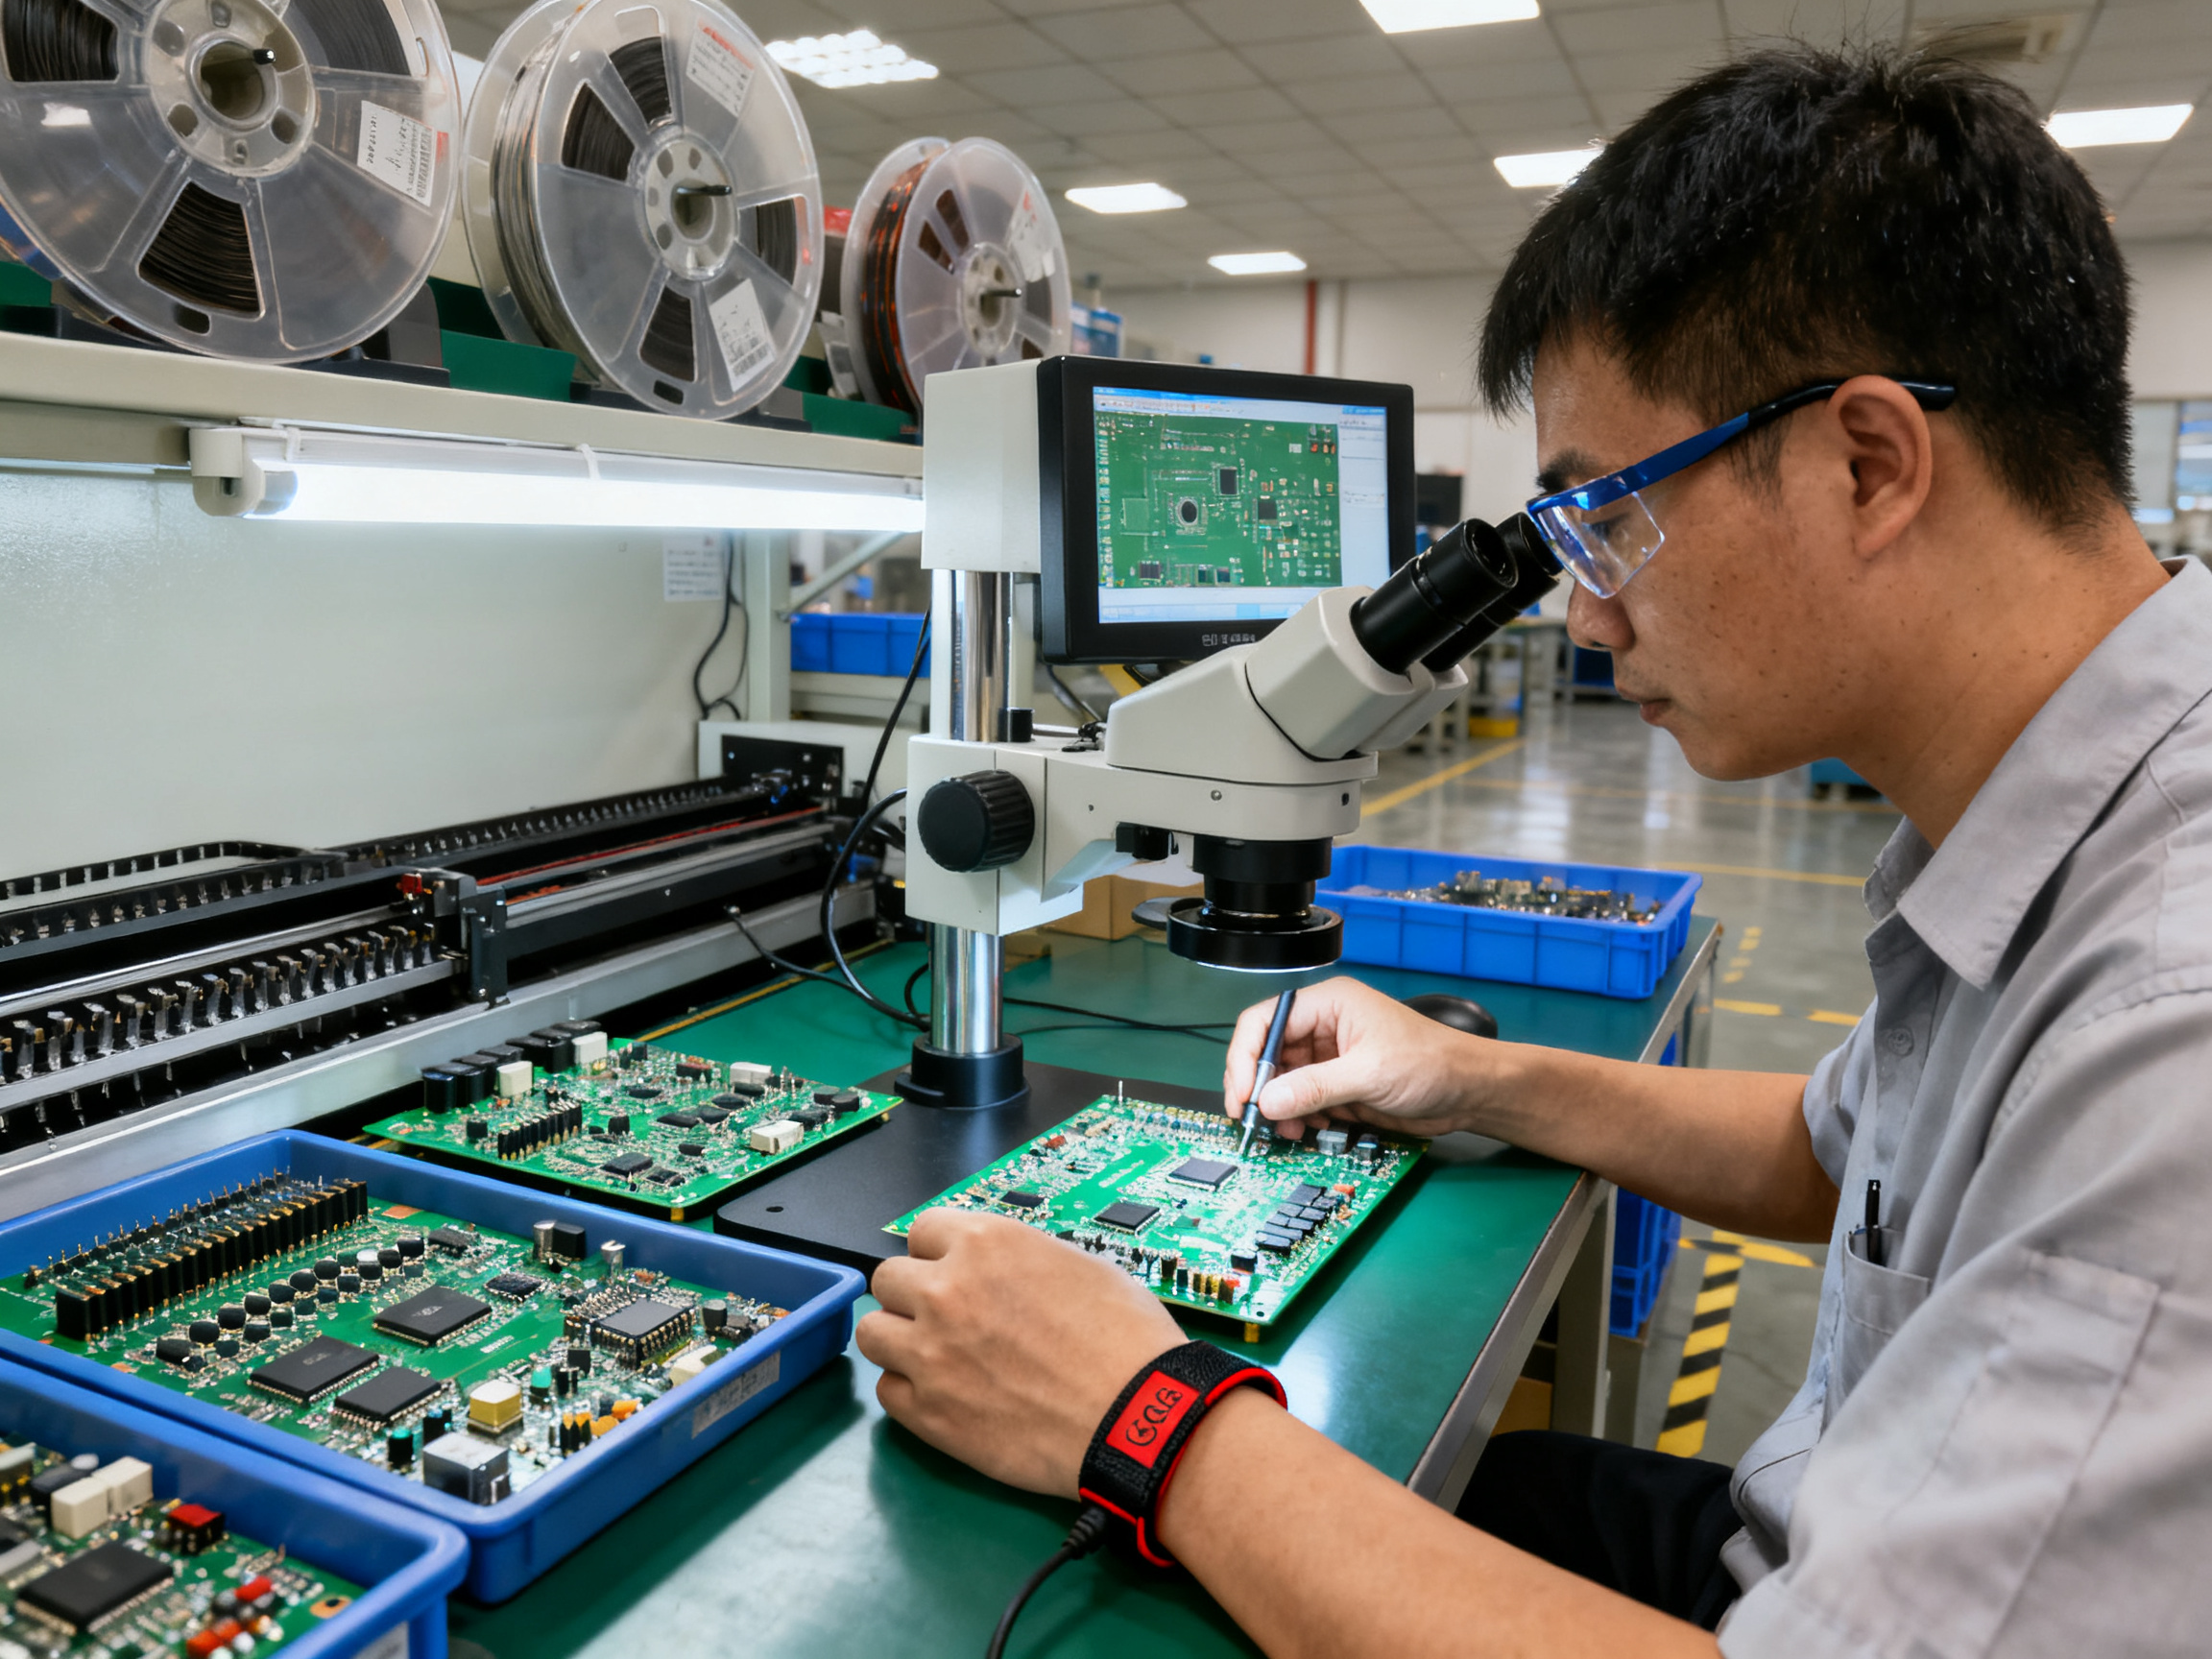
Visual inspection under magnification remains your first line of defense. Train your operators to recognize the common defect signatures: bridges between pads, icicles hanging from components, cold joints with dull or grainy surfaces, and any components that shifted during soldering. Make this a standard part of the production workflow, not a separate QC station that boards might skip.
Automated optical inspection (AOI) catches defects that human eyes miss, especially on high-volume lines where operator fatigue becomes a factor. Modern AOI systems from manufacturers like Shenzhen Chuxin Electronic Equipment Co., Ltd. include libraries specifically for wave solder defects, making setup straightforward for common board types.
For critical applications like automotive electronics, automated X-ray inspection (AXI) reveals internal joint quality that no optical system can see. Voids in solder joints, insufficient barrel fill in through-holes, and hidden bridges all show up clearly under X-ray. Budget for this capability if you’re serving automotive, aerospace, or medical customers.
Statistical Process Control for Wave Soldering
Statistical process control transforms quality from reactive troubleshooting into proactive prevention. By tracking your process parameters over time, you spot drift before it causes defects.
Key parameters to monitor include solder bath temperature, conveyor speed, wave height, preheat zone temperatures, and flux application rates. Record these values continuously if your machine supports it, or sample them at regular intervals if you’re working with older equipment.
Control charts help you distinguish between normal variation and genuine process shifts. When a parameter moves outside control limits, investigate immediately. Most shifts announce themselves gradually before they cause catastrophic problems.
| Parameter | Typical Control Limits | Sampling Frequency | Action if Out of Control |
|———–|———————-|——————-|————————-|
| Solder Bath Temp | ±5°C from setpoint | Continuous | Verify sensor, check heater |
| Conveyor Speed | ±10% from target | Every 2 hours | Recalibrate, check motor |
| Wave Height | ±0.5mm from target | Every 4 hours | Adjust pump, check nozzle |
| Preheat Zone 1 | ±10°C from target | Every 2 hours | Check heaters, verify airflow |
| Flux Density | ±5% from target | Every 4 hours | Adjust viscosity, check spray |
Defect Root Cause Analysis
When defects occur, resist the temptation to make random adjustments and hope for the best. Systematic root cause analysis finds the actual problem so you can fix it permanently.
The fishbone diagram remains a useful tool for organizing potential causes. For wave soldering, typical categories include machine parameters, materials (solder, flux, boards), methods (procedures, training), and measurement (calibration, inspection).
For recurring defects, collect data systematically. Track which shifts produce defects, which operators are running when problems occur, and whether there’s any correlation with material lots. This information narrows your search considerably.
From Our Experience: We worked with a manufacturer who kept seeing intermittent bridging on one specific board type. After two weeks of tracking, they noticed it always happened on second shift. Investigation revealed that one operator was running the conveyor 15% faster than specification during changeovers to make quota. The faster speed created insufficient dwell time, leading to bridges on the more complex areas of the board. Training and procedure changes eliminated the issue completely.
Continuous Improvement Framework
World-class manufacturers treat their processes as perpetually improvable. Even when you’re meeting quality targets, there’s usually room to reduce cost, increase throughput, or improve consistency.
Establish regular improvement cycles. Monthly, review your defect data and identify the biggest opportunities. Pick one or two to address, implement changes, measure results, and standardize what works.
Cross-functional teams often see solutions that siloed groups miss. Include operators, process engineers, quality technicians, and even customers when appropriate. Fresh perspectives break through the assumptions that limit improvement.
Document everything you learn. When someone leaves, their knowledge shouldn’t leave with them. Build a knowledge base of setups, defect solutions, and improvement wins that future team members can reference.
Quality Metrics That Matter
Track defects per million opportunities (DPMO) as your primary quality metric. Well-controlled wave soldering typically achieves 500 to 2,000 DPMO. Tight process control can push this to 250 DPMO, and truly world-class operations hit 50 DPMO or better.
First-pass yield measures how many boards complete the wave solder process without any rework. Target 98% or higher for standard applications, and 99.5% or better for automotive and aerospace work.
Cost per defect includes not just the direct rework expense but also the hidden costs: labor for sorting and reinspection, delayed shipments, customer complaints, and potential warranty claims. When you calculate the true cost of defects, improvement investments often pay back quickly.
| Quality Metric | Acceptable | Good | World-Class |
|—————|————|——|————-|
| DPMO | <2,000 | <500 | <50 |
| First-Pass Yield | >96% | >98% | >99.5% |
| Cost of Quality | <3% of COGS | <1.5% | <0.5% |
| Customer Complaints | <100 ppm | <20 ppm | <5 ppm |
Building a Quality Culture
Technical systems matter, but people make quality happen. Build a culture where everyone takes responsibility for the work leaving their area.
Empower operators to stop the line when they see quality problems. A brief stop to address an issue costs far less than a batch of scrap or field returns.
Recognize and reward good quality work. People respond to positive reinforcement more sustainably than negative consequences.
Invest in training that goes beyond procedure memorization. When operators understand why processes work the way they do, they become partners in quality rather than just step-followers.
Quality control isn’t about finding bad work—it’s about building good work consistently. Put the systems, metrics, and culture in place, and your wave soldering operation will deliver reliable results shift after shift.
Step 10: Maintain Equipment for Long-Term Reliability
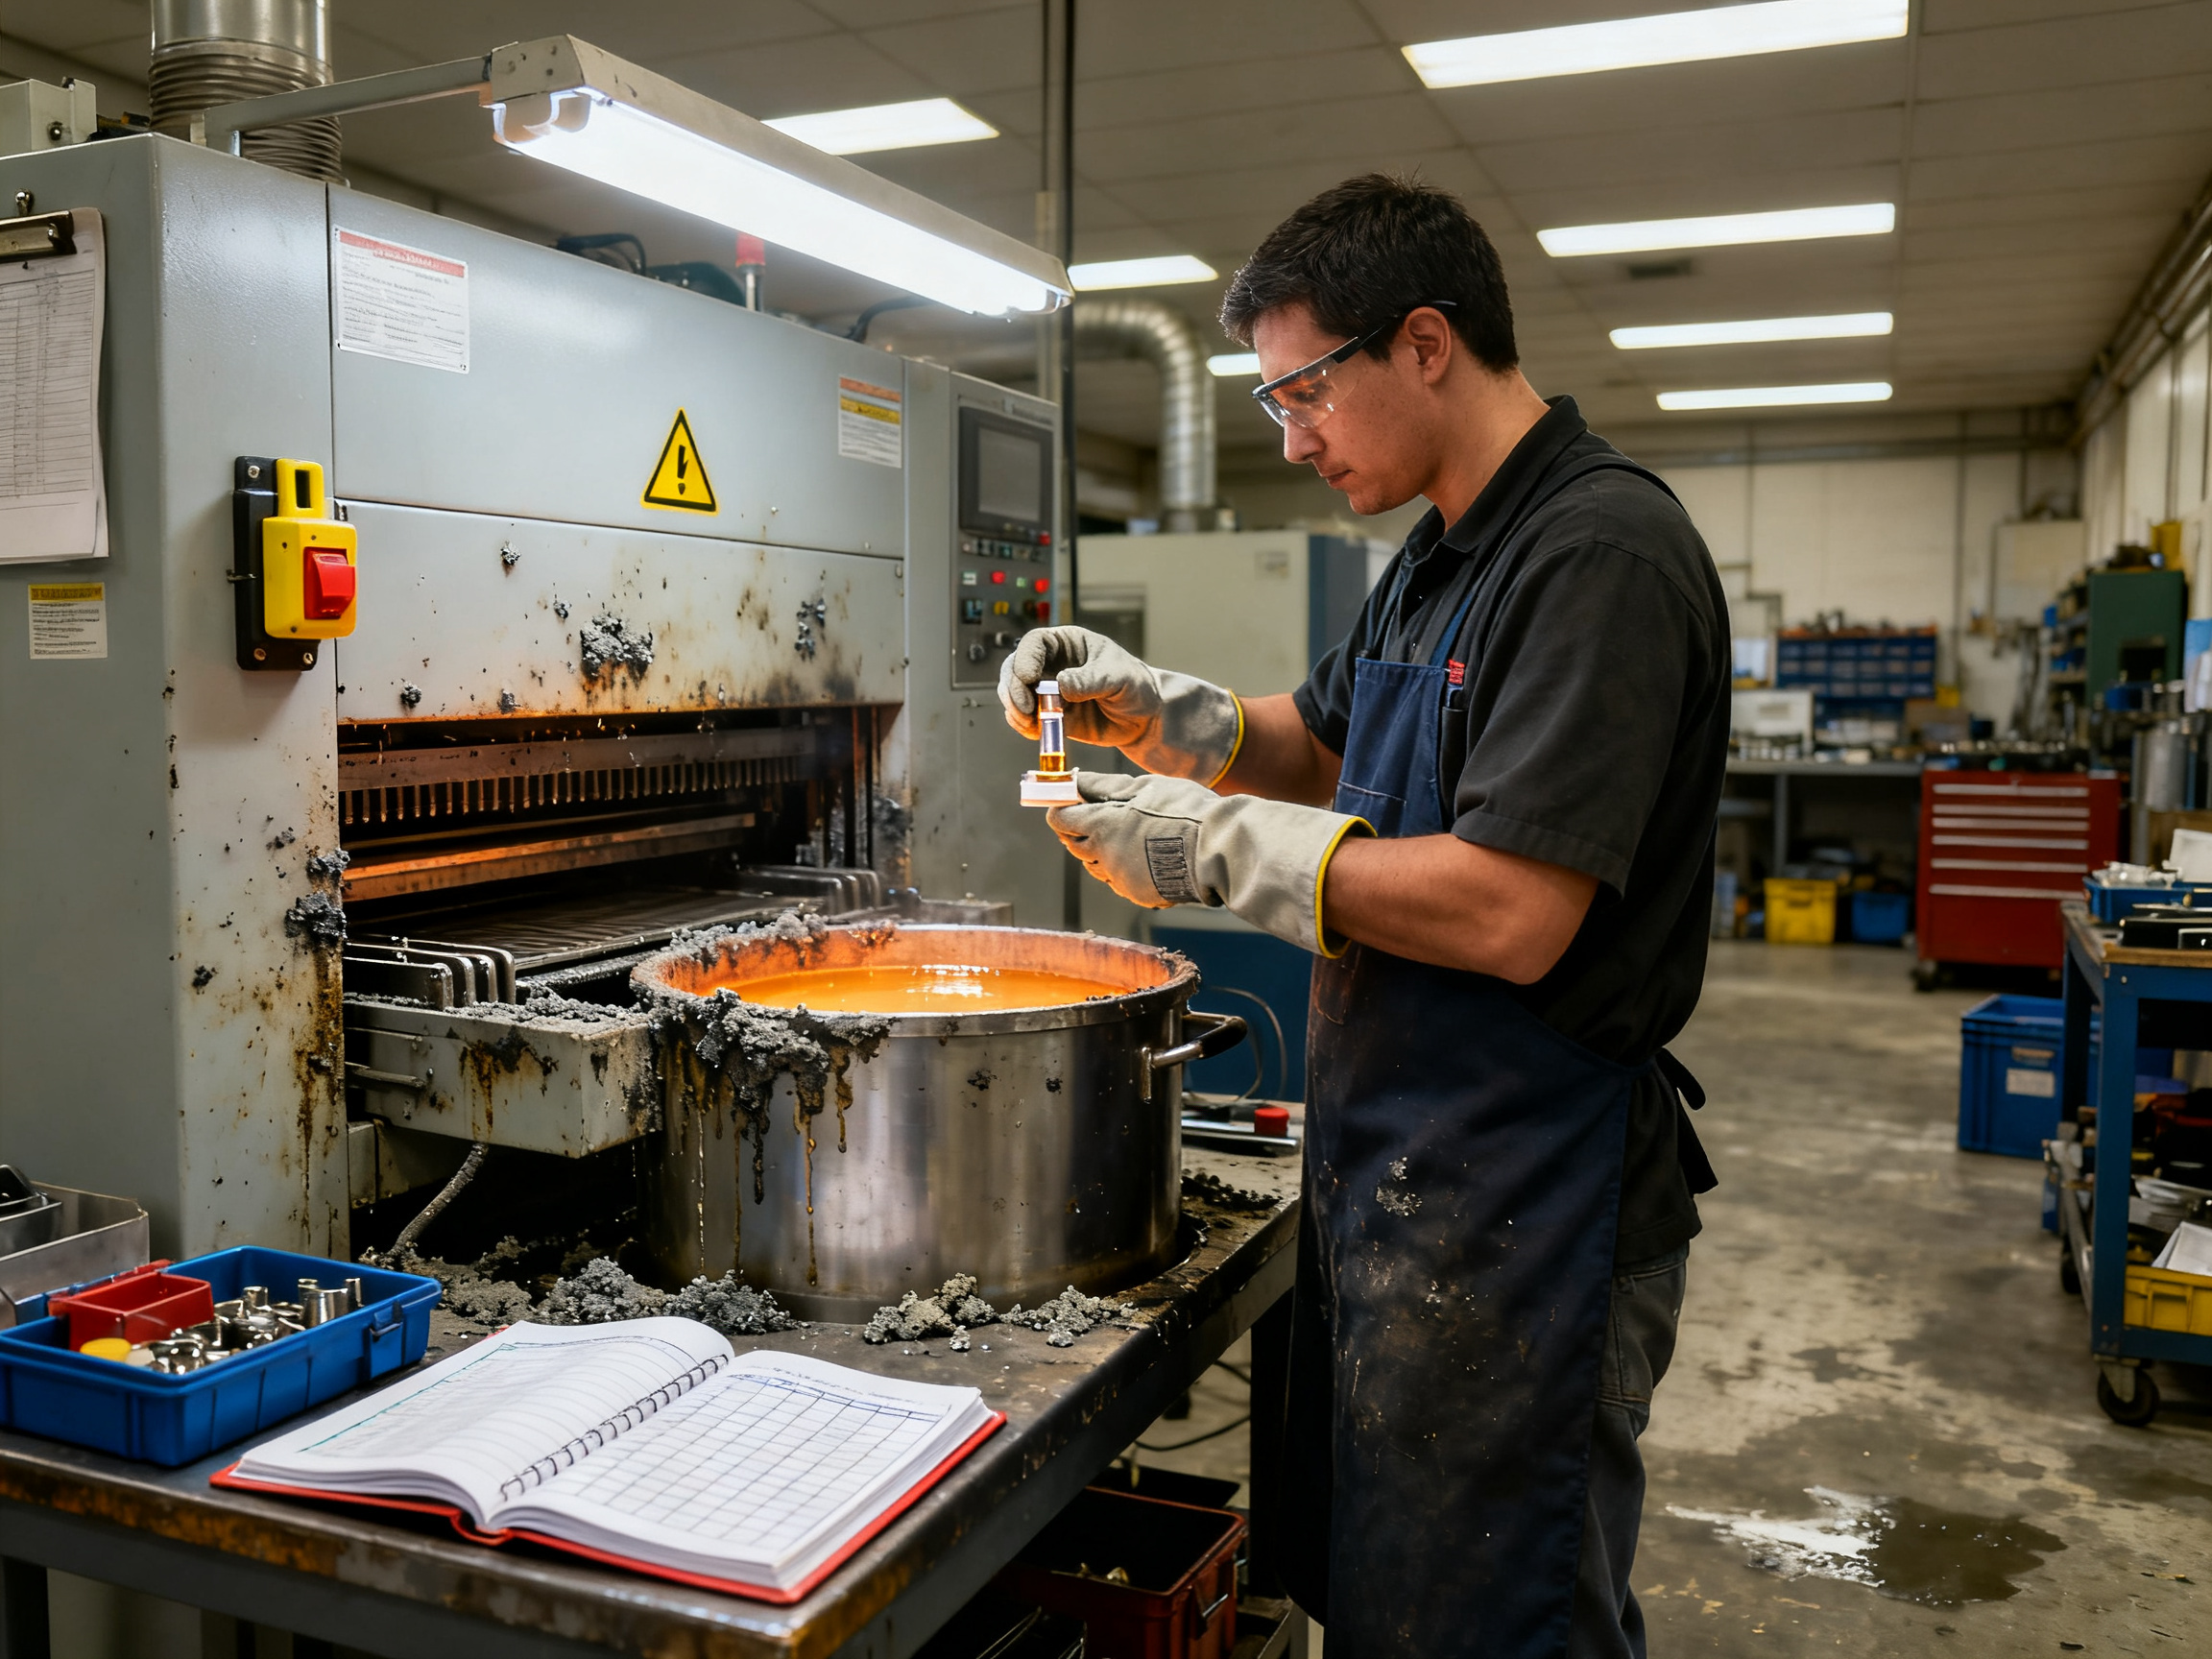
Your wave solder machine represents a significant capital investment, and protecting that investment means keeping up with maintenance. A well-maintained machine runs better, lasts longer, and produces more consistent quality than one that’s been neglected.
Preventive Maintenance Schedule
Preventive maintenance prevents problems before they interrupt production. Build a schedule that covers daily, weekly, monthly, and quarterly tasks, and stick to it religiously.
Daily checks take just a few minutes but catch issues before they escalate. Verify solder bath level and top up as needed. Check that emergency stops function correctly. Confirm that fume extraction is operating at proper flow rates. These quick checks cost almost nothing in time and prevent expensive surprises.
Weekly maintenance includes more thorough inspections of moving parts and cleaning. Check conveyor belt tension and alignment. Inspect wave nozzles for buildup or damage. Clean flux application systems and verify spray patterns. Remove dross from the solder bath surface.
Monthly tasks go deeper. Inspect and clean heating elements. Check thermocouple accuracy against a calibrated reference. Examine conveyor chains or belts for wear. Verify that all safety interlocks function correctly. Calibrate flux density measurement equipment.
Quarterly and annual maintenance addresses components that wear slowly over time. Replace worn conveyor components. Check electrical connections for security and corrosion. Have temperature controllers professionally calibrated. Consider annual service from your equipment vendor for comprehensive assessment.
| Maintenance Level | Key Tasks | Time Required | Frequency |
|——————|———-|—————-|———-|
| Daily | Level check, safety test, flow verification | 10-15 minutes | Every shift |
| Weekly | Conveyor check, nozzle inspection, system clean | 30-45 minutes | Weekly |
| Monthly | Heating elements, thermocouples, calibration | 1-2 hours | Monthly |
| Quarterly | Wear parts, electrical inspection, deep clean | 2-4 hours | Quarterly |
| Annual | Professional service, comprehensive calibration | 4-8 hours | Annually |
Solder Bath Maintenance Protocol
The solder bath requires special attention because its condition directly affects joint quality. Regular maintenance keeps composition stable and minimizes dross formation.
Monitor copper content continuously or at every shift. When copper exceeds your alloy’s tolerance, take action. Partial drain and top-up with fresh solder restores proper composition. Full bath change may be necessary if contamination becomes severe.
Dross removal should happen every 2 to 4 hours of operation, more often if you’re running without nitrogen inerting. Skim the surface gently without stirring dross back into the bath. Use proper tools designed for this task—improvised implements can introduce contaminants.
When changing the bath completely, clean the tank thoroughly before adding fresh solder. Remove all old alloy, flux residue, and any accumulated debris. Inspect the tank for damage or corrosion while it’s empty. A clean start gives you the best foundation for quality production.
Conveyor System Care
Conveyor problems create some of the most frustrating and costly downtime in wave soldering. Belt tracking issues, motor failures, and guide misalignment all bring production to a halt.
Keep guides and rails clean and properly aligned. Debris buildup causes boards to bind or mistrack. Check edge clearance regularly—components hanging over board edges can catch on guides and cause jams.
Monitor belt tension and condition. Too loose causes slipping and inconsistent speed. Too tight accelerates wear on bearings and motors. Follow manufacturer specifications for tensioning.
Lubricate moving parts according to the maintenance schedule. Use only approved lubricants—some common oils react with flux chemistry and create contamination problems.
Heating System Maintenance
Heaters and temperature control systems affect both quality and energy efficiency. Neglected heating systems consume more power and produce inconsistent results.
Check heating element resistance periodically. Elements that have lost significant output still heat but draw more current and fail sooner. Replace elements before they fail completely.
Inspect thermocouples for drift or damage. Calibration drift of even a few degrees creates process problems that are hard to diagnose. Replace thermocouples on schedule even if they seem to be working.
Clean heating zones of flux residue and dross accumulation. Contamination on heating surfaces acts as insulation, reducing efficiency and creating hot spots.
Spare Parts Strategy
Keep critical spare parts on hand to minimize downtime when failures occur. The exact parts depend on your machine model, but common items include thermocouples, fuses, pump seals, conveyor belt sections, and flux system components.
Build a relationship with your equipment vendor for emergency parts orders. Understanding which parts have long lead times helps you prioritize inventory.
Track failure patterns to anticipate future needs. If a particular component fails regularly, stock more of them and investigate why they fail prematurely.
Documentation and Records
Every maintenance activity should be documented. Records serve multiple purposes: they prove that maintenance was performed, help identify patterns in equipment behavior, and provide valuable information when troubleshooting problems.
Use a computerized maintenance management system (CMMS) if your operation is large enough to justify it. Even a simple logbook works for smaller operations—consistency matters more than complexity.
Record what was done, who did it, when it was completed, and any observations about equipment condition. This information builds a history that helps predict future maintenance needs and diagnose intermittent problems.
Proper maintenance transforms wave soldering from an unpredictable process into a reliable one. Invest the time and resources to maintain your equipment, and it will reward you with consistent quality and long service life.
Conclusion: Mastering Wave Soldering Through Systematic Excellence
Wave soldering remains a critical process in electronics manufacturing, despite decades of predictions about its decline. Through-hole components persist in many applications, and mixed-technology assemblies continue to require the robust joints that wave soldering provides.
This guide has walked through the complete wave soldering setup and operation process, from initial requirements assessment through long-term maintenance. The step-by-step approach ensures that nothing gets overlooked during implementation.
The fundamentals matter most. Proper solder bath temperature and composition create the foundation for good joints. Correct conveyor speed and wave height ensure proper contact and drainage. Appropriate preheat protects components and activates flux effectively. Well-configured flux application enables clean, reliable wetting.
But technical setup alone doesn’t guarantee success. Integration with your production line, systematic quality control, and continuous improvement practices separate acceptable operations from excellent ones.
Most importantly, your people make the difference. Invest in training that builds genuine understanding of the process. Empower operators to make good decisions. Recognize and reward quality work. Create a culture where everyone takes responsibility for the assemblies that bear your company’s name.
The electronics industry continues to evolve. New alloys, new components, and new applications create ongoing challenges. But the principles of good wave soldering remain constant: control your parameters, monitor your processes, and never stop improving.
Your wave soldering operation has the potential to achieve defect rates well below 100 DPMO—levels that seemed impossible a decade ago. The gap between good and world-class performance comes down to attention to detail, systematic process control, and the relentless pursuit of improvement.
Now get out there and build something great. Your next perfect solder joint is waiting.
Step 9: Train Operators and Establish Standard Operating Procedures
Your machine could be perfectly configured, your solder bath at ideal temperature, and your conveyor dialed in just right. But if your operators don’t know how to run it consistently, none of that matters. Training and standard operating procedures form the backbone of repeatable quality in wave soldering operations.
Let’s be real about this. The difference between a shop that fights the same problems every shift and one that runs smoothly comes down to how well people understand what they’re doing and why.
Developing Comprehensive Standard Operating Procedures
Good SOPs document everything your team needs to know about wave soldering setup and operation. That means step-by-step instructions for daily startup, normal operation parameters, changeover procedures, and shutdown. Include troubleshooting guides for the defects most likely to occur on your specific products.
Here’s something most shops miss. Your SOPs should explain the why behind each step, not just the what. When operators understand why solder bath temperature matters or why preheat matters so much, they’re better equipped to spot problems before they become defects.
For regulated industries like automotive and aerospace, your documentation needs to meet specific standards. ISO 9001 requires proof that operator competence is planned, delivered, evaluated, and retained as records. IATF 16949 for automotive goes further with job-specific skill matrices tied to your control plan and process risks.
IPC-A-610 remains the workmanship standard that defines what’s acceptable for electronic assemblies. Make sure your training covers the solder joint acceptance criteria your customers expect.
Training Operators Effectively
Build a training program that covers machine setup basics, solder pool and temperature control, conveyor speed adjustment, flux handling, component orientation, defect recognition, ESD control, safety procedures, and IPC-A-610 workmanship standards.
Theory alone isn’t enough. Hands-on practice on actual equipment builds real competence. New operators should work alongside experienced ones until they’ve demonstrated ability to run production independently.
Track training completion for every operator. Document when training happened, what it covered, and who confirmed competency. This protects you when problems occur and proves to customers that your team is qualified.
Training Competency Checklist
| Competency Area | Topics to Cover | Assessment Method | Valid Until |
|—————-|—————–|——————-|————-|
| Safety | PPE use, emergency procedures, fume hazards | Written test + observation | Annual |
| Machine Operation | Startup, shutdown, normal parameters | Hands-on demonstration | 2 years |
| Setup Procedures | Recipe changes, wave height, conveyor speed | Performance under supervision | 1 year |
| Defect Recognition | Bridges, cold joints, icicles, tombstoning | Visual inspection test | 1 year |
| Troubleshooting | Common problems, escalation path | Scenario-based assessment | 2 years |
| Documentation | Log entries, nonconformance reporting | Review of actual records | 1 year |
Industry Certifications Worth Pursuing
Beyond internal training, industry certifications add credibility. IPC certification validates your team’s knowledge of workmanship standards. Some manufacturers specifically require IPC-certified operators for automotive and aerospace work.
Your equipment vendor probably offers training specific to their machines. Shenzhen Chuxin Electronic Equipment Co., Ltd. provides operation training that helps your team get the most from their wave solder equipment. This training pays for itself quickly through reduced setup time and fewer defects.
Schedule regular refresher training, especially when you change materials, add new products, or see quality problems indicating a skill gap. A little ongoing investment in your people delivers huge returns in consistent quality.
Step 10: Implement Ongoing Monitoring and Optimization
Your wave soldering setup isn’t a set-it-and-forget-it situation. Even after you nail the perfect parameters, things drift. Temperature sensors get slightly off, conveyor belts stretch, flux formulations change slightly between batches. That’s why ongoing monitoring matters so much.
Real-time monitoring catches drift before it becomes defects. Modern equipment like Shenzhen Chuxin Electronic Equipment Co., Ltd. machines include sensor systems that track critical parameters throughout production. But having the sensors isn’t enough. You need to actually watch the data and respond when things move outside acceptable ranges.
Critical Parameters to Track
The big three you can’t ignore: solder bath temperature, conveyor speed, and wave height. These directly affect every joint your machine makes. Temperature drift of just 5 degrees can shift your wetting behavior enough to cause problems. Conveyor speed affects dwell time, and dwell time directly ties to hole fill and joint quality.
From Our Experience: We had a customer running wave soldering for six months without any issues, then suddenly defect rates spiked 3% across three shifts. Turns out their solder pot thermocouple had drifted 12 degrees out of spec. Nobody was checking the actual temperature versus the displayed temperature. After we implemented a simple twice-daily manual verification check against a calibrated pyrometer, that problem disappeared. Basic stuff, but it saved them thousands in scrap.
Beyond the primary parameters, flux density and nitrogen flow rates deserve attention. These indirectly impact joint quality by affecting oxidation and wetting behavior.
Maintenance Schedule Template
| Task | Frequency | Key Checks | Expected Time |
|——|———–|————|—————|
| Temperature verification | Twice daily | Manual pyrometer check vs display | 5 minutes |
| Conveyor speed check | Daily | Strobe tachometer reading | 3 minutes |
| Wave height inspection | Weekly | Physical measurement with gauge | 10 minutes |
| Flux density test | Every 4 hours | Viscosity cup reading | 5 minutes |
| Dross removal | Every 2-4 hours | Skim surface, check level | 15 minutes |
| Full process audit | Monthly | Cpk calculation, defect analysis | 2 hours |
| Equipment service | Quarterly | Vendor inspection, calibration | 4 hours |
Expert Tip: Build your monitoring routine around actual risk, not arbitrary schedules. High-volume lines making automotive or aerospace products need tighter monitoring intervals than low-volume consumer work. Adjust your frequency based on what happens when something drifts.
SPC and Process Audits
Statistical process control transforms your monitoring from reactive to proactive. Instead of finding problems after they happen, SPC helps you spot trends that predict problems before defects appear.
Track your critical parameters on control charts. Set upper and lower control limits based on your process capability. When a parameter approaches limits, investigate before it breaches them.
Regular process audits dig deeper than routine monitoring. Monthly, review your defect data by type, shift, and product family. Look for patterns. Sometimes the biggest improvements come from questions like “why does Tuesday afternoon always run worse than Monday morning?”
KPI Dashboard Example
| KPI | Target | Current | Status |
|—–|——–|———|——–|
| DPMO | <100 | 67 | Green |
| First-Pass Yield | >99% | 98.7% | Yellow |
| Solder Bath Temp | 260C +/-5 | 259C | Green |
| Conveyor Speed | 1.2 m/min +/-10% | 1.18 m/min | Green |
| Wave Height | 12mm +/-0.5mm | 12.2mm | Green |
| Downtime | <2% | 1.4% | Green |
Review this dashboard every shift. When something turns yellow, that’s your signal to investigate. Don’t wait for it to go red and defects to start showing up.
The goal here is continuous improvement. Your 2026 target should be pushing toward that 50 DPMO world-class benchmark. Every improvement in monitoring, every drift caught early, gets you closer.
Conclusion: Optimizing Your Wave Soldering Operation for Competitive Advantage
Getting your wave soldering operation right creates ripples across your entire business. Quality improves, costs drop, and your customers notice the difference in ways that translate directly to your bottom line.
The manufacturers pulling ahead in 2026 share some common traits. They treat wave soldering as a strategic capability, not just a production step. They invest in proper equipment from reputable suppliers, train their people thoroughly, and monitor their processes obsessively. They use statistical process control and modern inspection technology to catch problems before defects escape.
The data backs this up. Well-controlled wave soldering lines hit 500 to 2,000 DPMO consistently. With tighter control and modern equipment, that drops to 250 DPMO. World-class operations shoot for 50 DPMO or better. Those numbers represent real money saved on rework, warranty claims, and customer complaints.
Key Setup Parameters Quick Reference
| Parameter | Standard Range | Target | Monitoring Frequency |
|———–|—————|——–|———————|
| Solder Bath Temperature (SAC305) | 255 to 265 degrees C | Set point plus/minus 5 degrees | Continuous |
| Conveyor Speed | 1.0 to 1.5 m/min | Per recipe specification | Every 2 hours |
| Wave Height | 50 to 67% of board thickness | Consistent crest contact | Every 4 hours |
| Preheat Temperature | 100 to 150 degrees C | Even across board surface | Every 2 hours |
| Dwell Time | 2 to 6 seconds | Recipe-dependent | First article verification |
| Flux Application | 20 to 60 g/m2 | Uniform coverage | Every 4 hours |
Next Steps for Your Operation
Start by auditing your current setup against the parameters in this guide. Pick the two or three biggest gaps and address those first. Build from there.
Consider bringing in your equipment vendor for a process review. Companies like Shenzhen Chuxin Electronic Equipment Co., Ltd. offer assessment services that often uncover opportunities your team might miss.
Invest in training if your operators are running on experience alone. IPC certification programs and vendor-specific training pay back quickly through reduced defects and faster changeovers.
Set up real-time monitoring if you have older equipment without it. Even basic data logging helps you spot drift before it causes problems.
Additional Resources
Bookmark IPC standards for your reliability class, especially IPC-A-610 for workmanship and J-STD-001 for process requirements. Your equipment vendor documentation covers your specific machine capabilities and recommended maintenance schedules.
The manufacturers who treat wave soldering as a core competency, not overhead, are the ones winning in competitive markets. Start optimizing today.
Strong process control separates acceptable results from excellence in electronics assembly.